


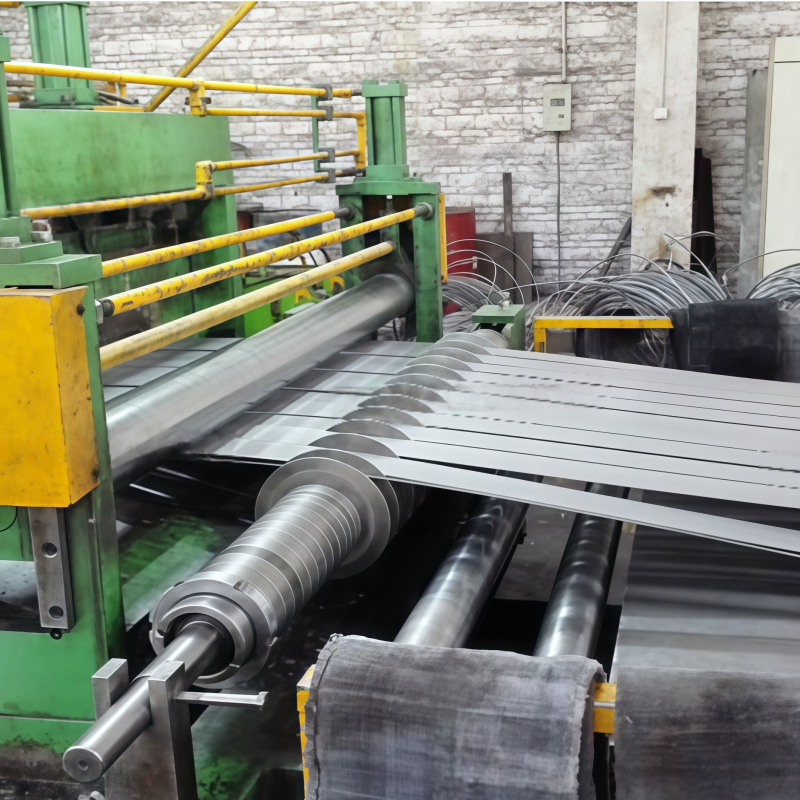
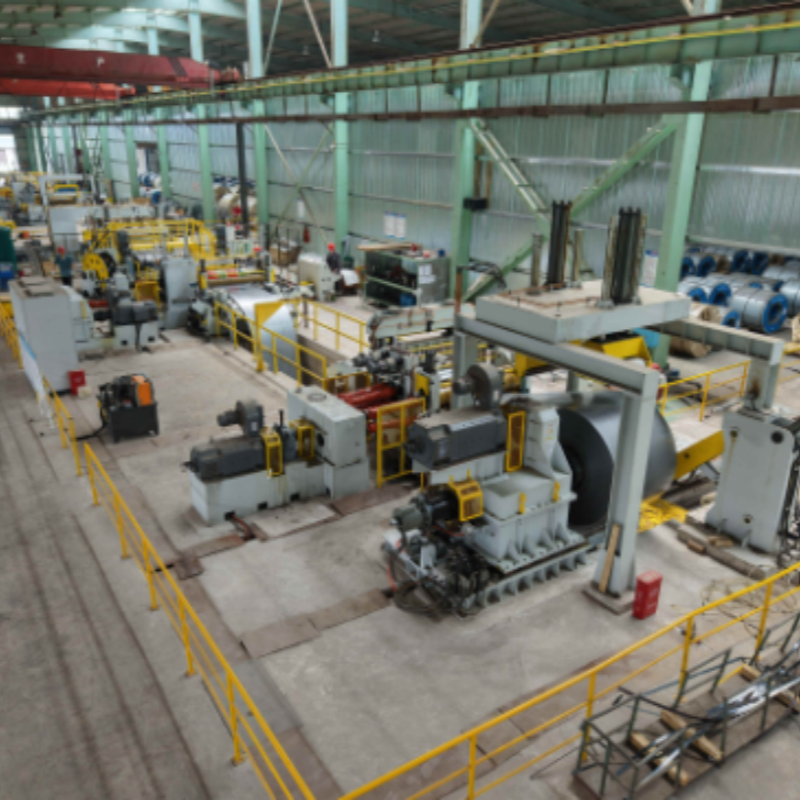
China Metal Slitting Machines Lines - Quality Products from Leading Suppliers and Factory
General Technical Requirements for Production Lines
The processing precision of the production line is in accordance with the relevant requirements of the “main technical parameters”. The seller is established on the basis of satisfying the buyer’s requirements and can make appropriate adjustments to the contents specified in the specification.
There is no abnormal vibration and noise for the product line and it should be in accordance with the requirements of the related state standards.
When hydraulic components and pressure station are normally operated and maintained according to Specifications, we make sure that it’s no leakage or natural damage. The replacement or maintenance should be supplied for the user in time.
Bead appearance of all the weld assemblies should be uniform in height and width. The connection between the weld assemblies and the parent metals should be transitioned smoothly. Getting rid of the splash and grinding are necessary to make the surface waviness nice and symmetry.
There is no crack, cold joint, slag inclusion, flame breakthrough, weld beading, undercut and air hole, etc. on the welded joint.
The appearance of the product line should be painted according to the user’s requirements.
Appearance of the paints: Oil film should be equal and there is no hanging stream, orange peel and pin-hole air bubble on it. Painting dressing surface shouldn’t show any trace of white.
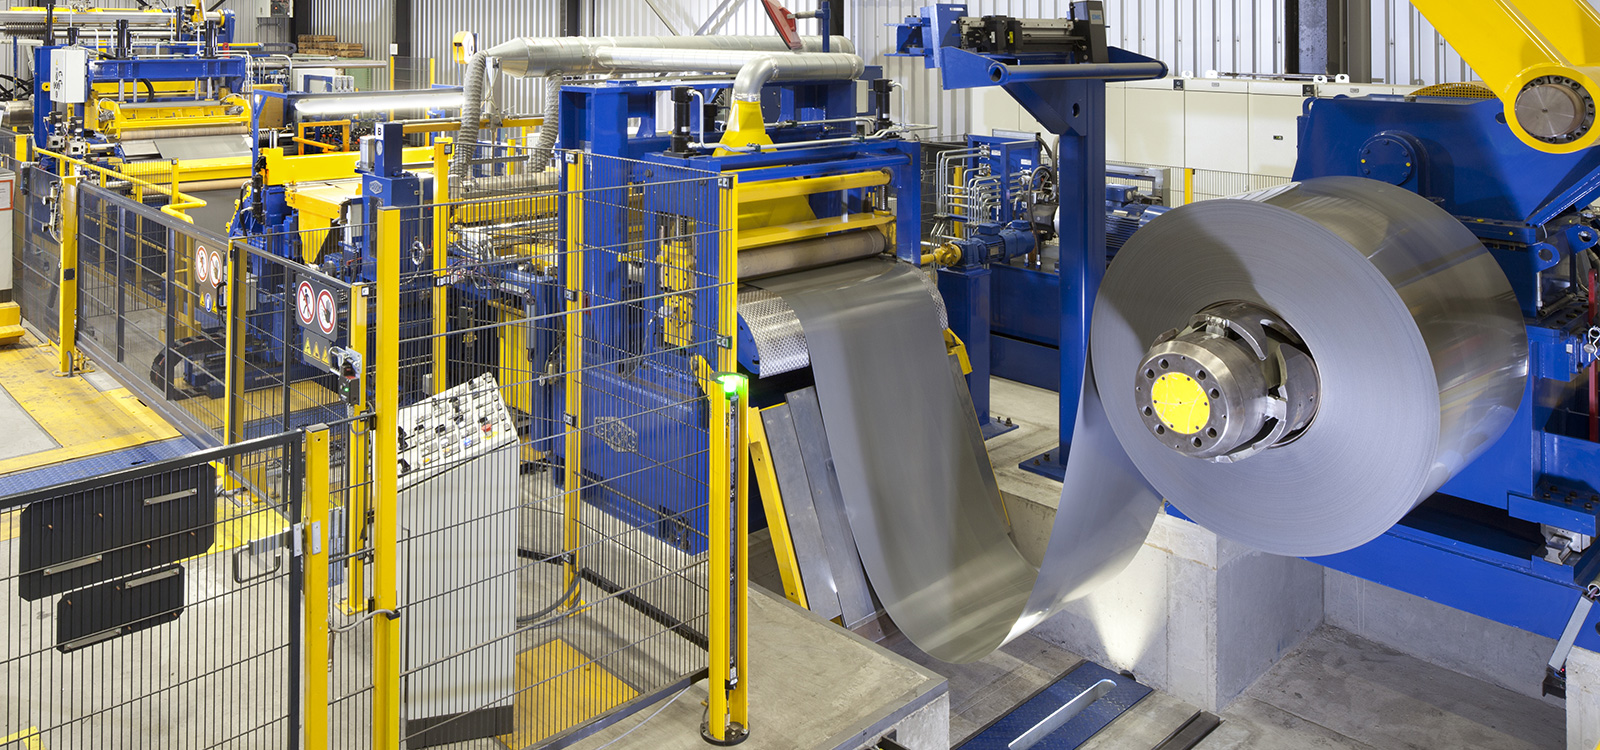
Working Processing
Key System Features
Capacity Estimation Table
| Capacity Estimation Table (Coil = 15t) | |||||||||
|---|---|---|---|---|---|---|---|---|---|
| NO | Thickness | Width | Coil Length | Slitting Speed | Time to Slitting | Auxiliary Time | Full Time per Coil | Annual Working Time Fund | Annual Productivity |
| mm | mm | m | m/min | m/min | min | min | Hour | ton | |
| ① | ② | ③ | ④ | ⑤ | ⑥ | ⑦ | ⑧ | ⑨ | ⑩ |
| 1 | 1 | 1250 | 1538.46 | 120 | 13 | 20 | 33 | 6000 | 163,636 |
| 2 | 2 | 1250 | 769.23 | 100 | 8 | 20 | 28 | 6000 | 192,857 |
| 3 | 3 | 1250 | 512.82 | 100 | 6 | 20 | 26 | 6000 | 207,692 |
| 4 | 4 | 1250 | 384.61 | 80 | 5 | 20 | 25 | 6000 | 216,000 |
| 5 | 5 | 1250 | 307.7 | 70 | 5 | 20 | 25 | 6000 | 216,000 |
|
Note: - The line operates 120 hours a week, i.e. 5 working days of 24 hours; - Auxiliary time is the preparatory and final time (time for installing and refilling the roll into the line and removing the roll from the winder, replacing cutting knives, etc.) Calculation of annual production: - Line ⑥ = Line ④ ÷ Line ⑤ - Line ⑦ = according to the Supplier - Line ⑧ = Line ⑥ + Line ⑦ - Line ⑩ = Line ⑨ x 60 ÷ Line ⑧ x 15 tons |
|||||||||
Motor Configuration and Power Meter of Main Equipment of the Unit
| NO | Name | Quantity | Motor Power (KW) | Remark | |
|---|---|---|---|---|---|
| AC | DC | ||||
| 1 | Coil Car | 1 | 3 | Coil car moving | |
| 2 | Uncoiler | 1 | 30 | Uncoil power | |
| 3 | Material guiding machine | 1 | 55 | Working roll driving | |
| 4 | Slitting machine | 1 | 160 | Working roll driving | |
| 1 | 1.1 | Upper roll lifting | |||
| 1 | 0.75 | Arch forth and back | |||
| 5 | Scrap winder | 2 | 7.5 | Scrap power | |
| 6 | Recoiler | 1 | 200 | Recoil power | |
| 7 | Unloading car | 1 | 3 | Coil car moving | |
| 8 | Hydraulic system | 2 | 22 | Cylinder driving | |
| Total | ≈ 510 KW | Flexible design | |||
Frequently Asked Questions (FAQ)
Inquire Now!
For inquiries about our products or pricelist, please leave your email to us and we will be in touch within 24 hours.