


 Tube Mill Consumables: Inspection & Replacement Guide




ERW Squeeze Force: Finding the Right Balance Between Welding Power and Pressure
ERW Squeeze Force: Why More Power Does Not Always Mean a Stronger Weld
Quick Answer: What Is the Correct Balance Between Power and ERW Squeeze Force?
Many engineers believe that increasing welding power can solve weak weld problems.
In reality, ERW welding quality depends on the balance between heat input and squeeze force.
Too much heat with insufficient pressure may trap molten oxides inside the weld.
Too little heat or inadequate squeeze force may create incomplete fusion and weak bonding.
A stable ERW weld requires the correct combination of welding temperature, V-angle, line speed, strip edge condition, and squeeze roller pressure. Studies of HF-ERW welding show that insufficient upset force can leave oxide inclusions inside the bond line, while process parameters such as heat input, welding speed, and squeeze force strongly influence weld defects.

Introduction
A tube can pass through the entire production line without any obvious warning signs.
The outside surface looks smooth.
The weld bead appears normal.
The dimensions meet the required tolerance.
Then the pipe enters a hydro test or flattening test, and the weld suddenly fails.
Many factories immediately check the high-frequency welder.
They increase the power.
They slow down the production speed.
They replace ferrite rods.
Sometimes the problem disappears for a short period of time.
A few coils later, the same defect returns.
This situation is common in ERW production.
The reason is simple: the welding system is not controlled by power alone.
The final weld quality is created by the relationship between heating and mechanical forging.
The squeeze rolls do not simply close the V-opening.
Their task is to apply enough force to remove molten oxides and forge two heated strip edges into one continuous metal structure.
When this balance is lost, defects begin to appear.
Some are visible immediately.
Others remain hidden until the pipe reaches a customer.
This is why experienced tube mill engineers do not ask only:
“How much power should we use?”
They ask a more important question:
“How does the welding power match the ERW squeeze force?”
Power Too High – When More Heat Creates a Weaker Weld
One of the most common mistakes in ERW production is assuming that a higher power setting always produces a stronger seam.
In fact, excessive heat can create a completely different set of problems.
When the strip edges remain at excessively high temperatures, the amount of molten material increases.
The V-shaped opening produces more oxides.
If the squeeze force is not high enough to expel these oxides, they become trapped inside the weld.
This defect is known as oxide inclusion.
The dangerous part is that the weld may still look acceptable from the outside.
The pipe may even pass visual inspection.
However, the internal structure is already weakened.
Research on HF-ERW welding shows that excessive heat input can change molten metal behavior and increase the possibility of defect formation when the balance between heat and metal expulsion is disturbed.
Typical Signs of Excessive Welding Power
Operators often observe:
- Large and irregular sparks
- Excessive external burr
- Burned weld edges
- High temperature around the squeeze point
- Increased oxide formation
Many factories try to solve poor welding by adding more power.
For a short time, the weld may appear stronger.
Later, hydro testing may reveal leakage or reduced mechanical performance.

Common Symptoms of Low Squeeze Force
- Hydro test failure
- Weak flattening test performance
- Incomplete fusion
- Internal oxide inclusion
- Low impact strength
Many operators continue adjusting electrical parameters when these defects appear.
However, the actual issue may be mechanical.
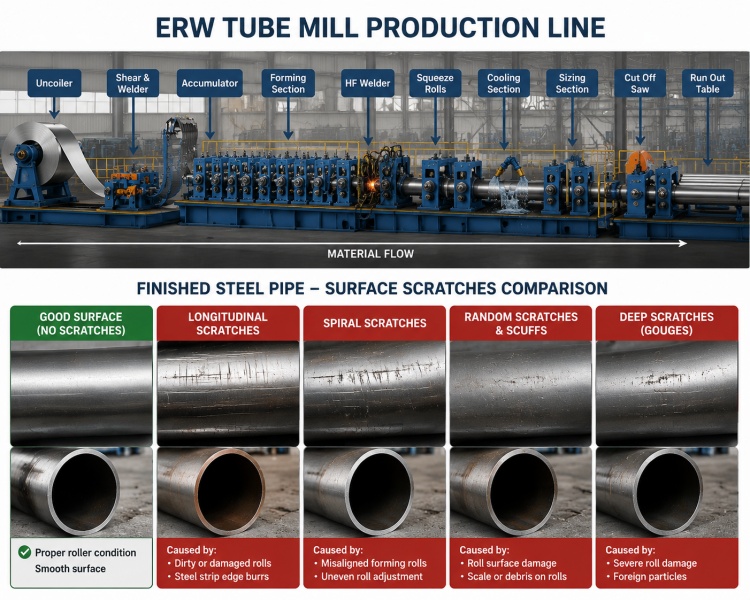
The squeeze roll alignment.
Bearing condition.
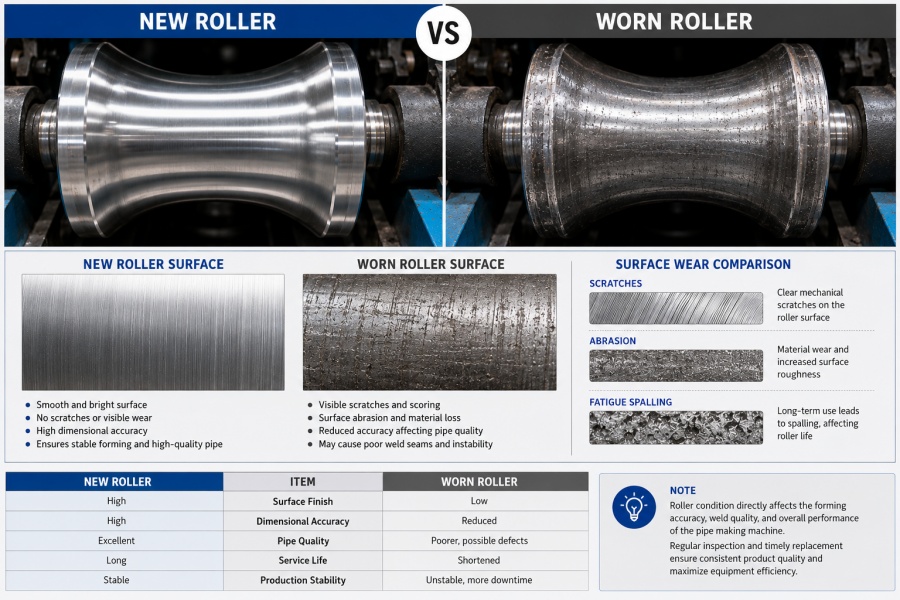
Roller wear.
Or incorrect squeeze adjustment.
Over Squeeze Problems — What Happens When Squeeze Force Is Too High?
Many tube mill operators believe that increasing squeeze roller pressure can solve weak weld problems.
However, this is one of the most common misunderstandings in HF ERW welding.
Too much squeeze force can damage the weld structure even if the welding power is sufficient.
Q: Can excessive squeeze force cause ERW pipe failure?
A: Yes. Over squeezing can create internal stress, excessive upset, and even cracks.
During high-frequency welding, the strip edges are heated to a plastic or semi-molten condition.
The function of the squeeze rolls is to apply the correct forging pressure so that impurities and oxides are expelled from the V-area and a solid metallurgical bond is created.
But when squeeze force is too high, several negative effects occur.
1. Excessive Weld Upset
A certain amount of upset is necessary because it pushes oxidized metal out of the weld centerline.
However, excessive upset means too much metal flow.
Common signs include:
- Large outside welding bead
- Excessive internal burr
- Uneven weld appearance
- Increased scarfing load
If the internal bead is not properly removed, it may affect the final application of the tube.
For example:
- Fluid transportation pipes may experience flow resistance.
- Precision tubes may fail dimensional requirements.

2. Formation of Residual Stress and Micro Cracks
Many manufacturers only check whether the pipe passes immediately after welding.
However, hidden problems may appear later.
Over squeezing can create:
- High residual stress
- Distorted metal flow lines
- Micro cracks near the weld zone
Research on HF-ERW tubes has shown that residual tensile stresses around the welded zone can contribute to failure during later flattening operations.
This means a pipe that looks perfect externally may still fail during quality testing.
3. Poor Results During Flattening Test
A common workshop situation:
“The weld looks good, hydro test passes, but flattening test shows cracks.”
This often confuses operators.
The reason may be that the welding process created a hard and brittle weld zone or excessive deformation.
Longitudinal cracks during flattening can be associated with excessive squeeze pressure, improper upset amount, or poor weld metal flow.
Best Welding Balance — Finding the Correct Relationship Between Power and Squeeze Force
The best ERW welding result does not come from maximum power or maximum pressure.
It comes from balance.
A successful weld requires:
Correct Heat Input
Too little heat:
- Cold welding
- Lack of fusion
- Weak bonding
Too much heat:
- Overheating
- Grain growth
- Excessive oxidation
Correct Squeeze Force
The squeeze rolls should provide enough pressure to:
✓ Remove oxides
✓ Forge two strip edges together
✓ Create a complete metallurgical bond
But not so much that:
✗ Excessive burr appears
✗ Metal flow becomes abnormal
✗ Residual stress increases
The Golden Rule in ERW Welding
Power provides the temperature.
Squeeze force creates the bond.
High power without enough squeeze gives a false weld.
High squeeze without proper heat creates stress and deformation.
Only a balanced combination gives a strong ERW seam.
H2: Hydro Test, Flattening Test, and UT Inspection — Which Defects Can They Find?
Many customers ask:
Q: If my pipe passes the hydro test, does it mean the weld is perfect?
A: No.
Hydro testing only verifies pressure tightness.
Some internal defects may not leak immediately but can appear under mechanical deformation or long-term service.
1. Hydrostatic Test
Purpose:
Check whether the pipe can withstand internal pressure.
It is especially effective for detecting:
- Through-wall cracks
- Pinholes
- Leakage paths
A pipe with porosity or through-thickness defects may fail hydro testing because water pressure reveals leakage channels.
2. Flattening Test
Purpose:
Evaluate weld strength and ductility.
Typical failures:
- Weld cracking
- Brittle fracture
- Poor fusion
A pipe may pass hydro testing but fail flattening because the weld lacks enough toughness or contains hidden defects.
3. Ultrasonic Testing (UT)
Purpose:
Detect internal defects without damaging the tube.
UT can identify:
- Lack of fusion
- Internal cracks
- Inclusions
- Voids
Modern ERW production lines often use online UT systems because many dangerous defects are invisible from the surface.
Real Field Experience — A Small Adjustment Saved Thousands of Dollars
One tube manufacturer producing 50 × 2.0 mm carbon steel pipes experienced repeated flattening failures.
The operators increased welding power several times.
The problem became worse.
After inspection, the actual cause was:
- Squeeze roll gap was too small.
- Excessive pressure caused abnormal metal flow.
- Large upset and residual stress developed around the weld.
The solution:
- Reduce squeeze pressure.
- Re-adjust V angle.
- Optimize HF power.
Result:
- Flattening pass rate increased.
- Scrap ratio dropped.
- Production became stable.
Lesson: More pressure does not mean a stronger weld.
Common Mistakes Operators Make in ERW Welding
Mistake 1: Increasing power whenever a defect appears
Not every weld defect is caused by insufficient heat.
- Worn squeeze rolls
- Incorrect alignment
- Improper pressure
Recommended reading:
Internal Link: Squeeze Roller Wear Issues and Solutions
Mistake 2: Using visual appearance as the only standard
A smooth external weld does not guarantee internal quality.
Always combine:
- Visual inspection
- Hydro test
- Flattening test
- UT inspection
Mistake 3: Ignoring Squeeze Roll Condition
A worn squeeze roll causes:
- Uneven pressure
- Poor edge contact
- Weld instability
Learn more:
【Internal Link: Tube Mill Squeeze Roller Maintenance Guide】
| Symptom | Possible Cause | Recommended Action |
|---|---|---|
| Weld opens during hydro test | Insufficient heat or lack of fusion | Increase power and check V angle |
| Flattening crack | Excessive squeeze or brittle weld | Reduce squeeze force and optimize heating |
| Large external burr | Too much squeeze | Adjust squeeze roll gap |
| Internal bead too high | Excessive upset or poor scarfing | Reduce pressure and adjust scarfing tool |
| Unstable weld quality | Worn squeeze rolls | Replace or regrind rolls |
| Frequent sparks at welding point | Improper heat balance | Check HF power and strip condition |
Recommended MIVI Tube Mill Solution
At MIVI, we understand that a stable ERW weld is not achieved by only having a powerful welding machine.
It requires a complete system including:
High Precision Squeeze Roll System
Advantages:
- Stable pressure transmission
- Accurate roll alignment
- Long service life
High Frequency Welding Machine
Advantages:
- Stable power output
- Efficient heating
- Better welding consistency
Professional Technical Support
Our engineers help customers:
- Adjust welding parameters
- Diagnose weld defects
- Optimize production efficiency
FAQ
Q1: Does higher squeeze force create stronger welds?
No.
Correct balance matters more than higher force.
Q2: Why does hydro test pass but flattening fail?
Hydro test checks leakage.
Flattening checks ductility and structural integrity.
Q3: How do I know squeeze force is too high?
Signs include:
- Large burr
- Difficult scarfing
- Flattening cracks
Q4: How often should squeeze rolls be checked?
Daily visual inspection is recommended.
Weekly detailed inspection is better for heavy production.
Conclusion
Squeeze rollers are among the most important components in ERW tube mills.
Their condition directly affects:
- Weld quality
- Production stability
- Product consistency
A perfect ERW weld depends on balancing:
- HF power
- V-angle
- Squeeze force
- Roll condition
- Line speed
Too little squeeze causes weak welds.
Too much squeeze creates stress and cracks.
The best welding performance comes from balance.
If your production line suffers from:
- Weld failure
- Excessive burr
- Hydro leakage
- Flattening cracks
- Unstable welding
It may be time to inspect your squeeze rollers.
Contact MIVI engineers to get a free ERW welding diagnosis and optimize tube mill performance
-
1. What is the material of the pipe that the machine produce
-
2. Is it possible to customize the equipment according to the demanding of the customer?
-
3. Do you have any certificates?
-
4. What is the payment method?
-
5. What does the after-service do you provide?
-
6. When will the engineer arrive?
-
7. How long will the installation and staff training?
-
8. Do you have reference project?
-
9. What about spare parts?
We will prepare enough spare parts for you to use. But these are consumables and need to be replaced regularly.