


 Tube Mill Consumables: Inspection & Replacement Guide




Five Proven Ways to Extend Tube Mill Roller Lifespan
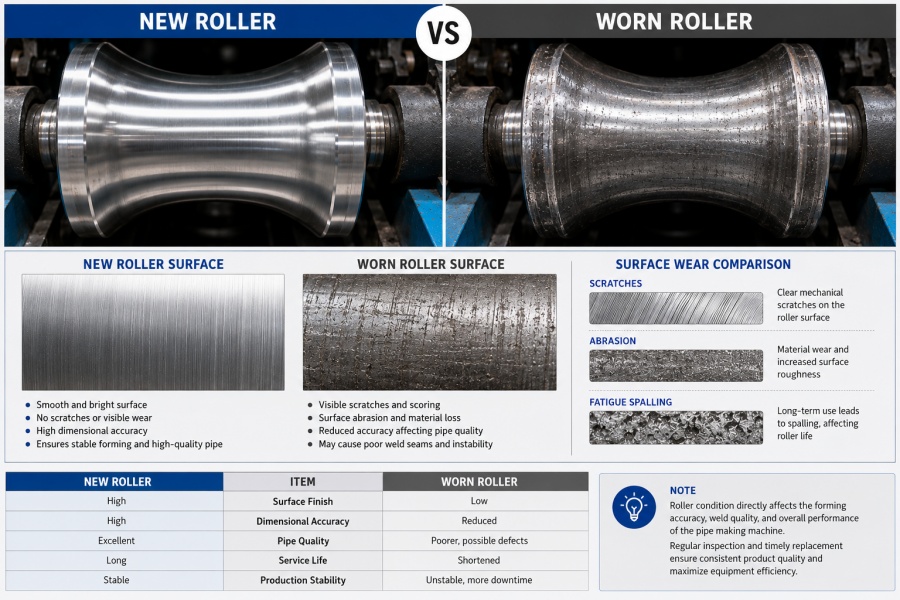
In modern steel pipe and tube manufacturing, tube mill rollers (forming, welding, and sizing rollers) represent a significant portion of operational expenditure. Unplanned roller wear, surface cracking, and deformation compromise pipe surface quality, cause dimensional deviations, and result in costly mill downtime.
Whether running high-speed carbon steel pipe mills or high-precision stainless steel tube lines, optimizing tube mill roller maintenance and selecting engineered metallurgy is essential for reducing total cost of ownership (TCO).
1. Ensure Precise Shaft Alignment and Pass Line Calibration
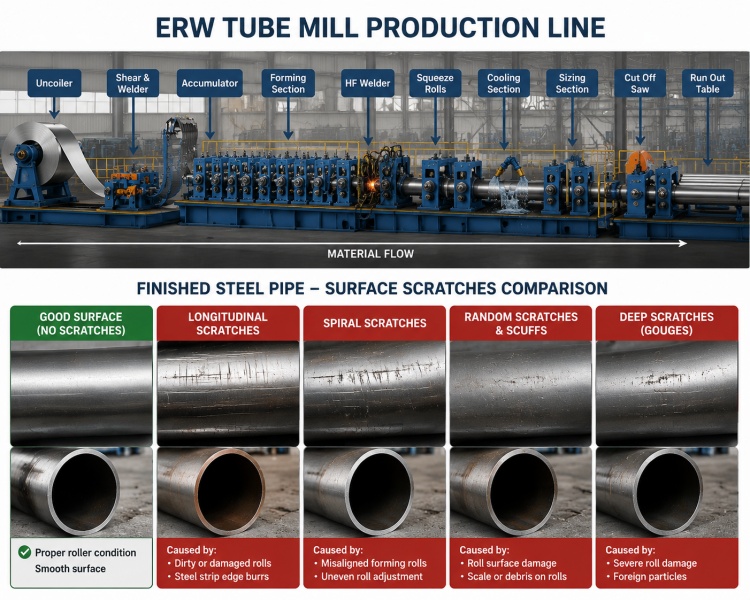
Improper roll setup and shaft misalignment are the leading causes of premature, asymmetrical roller wear. When forming and sizing rollers are off-center relative to the pass line:
- Localized Friction: Concentrated stress creates localized heat zones, accelerating groove wear on specific stands.
- Surface Defect Spikes: Misaligned rollers scrape the steel strip, leaving friction marks and scratches on finished tubes.
- Mechanical Strain: Axially unbalanced loads damage drive shafts, bearings, and stand housings.
Engineering Standard: Utilize laser alignment tools or German COPRA® roll design software protocols to verify shaft parallelism before every major production cycle. Maintaining a total pass-line alignment tolerance within ±0.05 mm distributes forming loads evenly across all stands.
2. Optimize Coolant Filtration and Thermal Management
High-speed roll forming generates immense friction heat at the contact point between the strip and the roller pass. Without continuous cooling and lubrication, thermal stress induces micro-cracking (thermal fatigue) on the roller surface.
To extend tube mill roller lifespan:
- Implement Magnetic Filtration: Fine steel scale and chips suspended in unfiltered coolant act as liquid abrasives. Install magnetic separators and 20-micron cartridge filters in your coolant reservoir.
- Use High-Performance Lubricants: Use synthetic or semi-synthetic coolants with extreme pressure (EP) and anti-rust additives.
- Optimize Nozzle Placement: Direct high-pressure coolant spray directly into the bite zone where deformation stress is highest.
3. Control Raw Material Edge Quality and Hardness
Your forming rollers interact directly with the incoming steel strip. Substandard coil preparation severely reduces roller longevity:
- Edge Burrs: Sharp burrs from poor slitting act as cutting edges, gouging the roller grooves. Ensure slitter knives are sharp and edge-trimming units upstream are functioning properly.
- Coil Hardness Spikes: Inspect incoming raw material for localized hard spots or un-pickled mill scale, which apply sudden impact loads to the roller profile.
4. Implement Preventive Wear Tracking & Re-Grinding Thresholds
Waiting for visible profile breakdown before servicing rollers often renders them irreparable. Establish a predictive maintenance schedule based on tonnage or operational hours:
- Routine Radius Checks: Use precision radius gauges and optical profilers during shift handovers to monitor groove expansion.
- Timely Re-Grinding: Schedule preventive re-grinding when wear depth reaches 0.15 mm–0.20 mm. Removing a minor layer of worn steel early preserves 90% of the roller material, allowing multiple re-grinding cycles over its lifetime.
5. Upgrade to Rollers Engineered with Advanced Vacuum Heat Treatment
While disciplined maintenance maximizes operational efficiency, the metallurgical foundation determines the ultimate ceiling of roller performance.
Standard surface-hardened or poorly tempered rollers wear rapidly under heavy continuous load. High-durability rollers require specialized tool steel chemistry combined with advanced thermal processing.
Technical Comparison: Standard Rollers vs. MIVI Precision Rollers
| Technical Parameter | Standard Market Rollers | MIVI High-Durability Rollers |
| Material Grade | Low-grade alloy / GCr15 / 45# Steel | Premium Cr12MoV, SKD11, D2, H13 |
| Heat Treatment Method | Basic Salt Bath / Surface Quenching | Vacuum Heat Treatment + Deep Cryogenic Processing |
| Hardness Uniformity | HRC 52–56 (Surface only) | HRC 60–63 (Uniform Core-to-Surface) |
| Machining Tolerance | ±0.03 mm – ±0.05 mm | CNC Precision Grinding within ±0.01 mm |
| Surface Finish | Ra 0.8 μm | Mirror Polished (Ra ≤ 0.2 μm) |
| Avg. Service Lifespan | Baseline (100%) | +30% to +50% Longer Lifespan |
Real-World Case Evidence
Field Test Result: A structural steel pipe manufacturer in South America experienced severe roller pitting every 45 days when running 3.0mm carbon steel tubes. After replacing their forming stands with MIVI SKD11 Vacuum Heat-Treated Rollers, average mill operational runtime increased from 45 days to over 110 days without re-grinding, reducing tooling costs by 38% annually.
Why MIVI Tube Mill Rollers Last Longer
At MIVI Machinery, an ISO9001:2015 certified manufacturer, we engineer custom forming, welding, sizing, and custom profile rollers engineered for heavy-duty industrial pipe production.
- Computer-Aided Profile Design: We utilize advanced CAD/CAM software to optimize flower patterns, minimizing material strain during roll forming.
- Proprietary Heat Treatment: Our vacuum furnace heat treatment combined with deep cryogenic tempering eliminates internal residual stress, preventing deformation and cracking under high load.
- Mirror Polishing Technology: All rollers for stainless steel and aluminum pipe mills undergo micro-polishing to prevent micro-scratches on sensitive tube surfaces.
By combining superior metallurgy with high-precision CNC machining, MIVI Tube Mill Rollers deliver exceptional resistance to impact, wear, and corrosion.
Frequently Asked Questions (FAQ)
Q1: What is the best steel material for tube mill rollers?
A: The best material depends on the application. For general carbon steel pipe production, Cr12MoV offers an ideal balance of wear resistance and cost. For heavy-duty forming or high-volume production, SKD11 (D2) is recommended due to its superior toughness and high carbon-chromium content. For stainless steel pipe mills, high-grade tool steel with mirror polishing or specialized coatings (such as TiN/TiALN) prevents surface galling.
Q2: How often should tube mill rollers be re-ground?
A: Rollers should be inspected every shift and scheduled for re-grinding once wear depth reaches 0.15 mm to 0.20 mm. Re-grinding early prevents micro-cracks from propagating deeper into the roller core.
Q3: Why do stainless steel pipes get surface scratches during roll forming?
A: Scratches are usually caused by friction heat, poor coolant filtration, or rough roller surface finishes. Using rollers processed with CNC mirror polishing (Ra ≤ 0.2 μm) and proper vacuum heat treatment prevents material transfer and scratch formation.
Conclusion
Extending your tube mill roller lifespan requires a two-fold approach: enforcing disciplined daily maintenance on your
Need Durable, High-Precision Rollers for Your Pipe Mill?
Stop suffering from frequent roller changes and high maintenance costs. Contact