


 Tube Mill Consumables: Inspection & Replacement Guide




How Squeeze Roller Wear Causes Weld Defects in ERW Tube Mills
Steel tube factories usually don’t stop production because of one dramatic failure.
Most of the time, problems begin with small changes nobody pays enough attention to.
The weld seam becomes slightly unstable.
Operators start adjusting welding current more often.
Rollers feel hotter than usual.
A faint vibration appears around the squeeze section.
Then one day the weld cracks during hydro testing.
Or the seam opens after flattening.
And suddenly the problem that looked “minor” turns into scrap, downtime, and customer complaints.
In many ERW tube mills, squeeze roller wear sits right at the center of those issues.
Not because the roller itself is expensive.
But because unstable squeeze pressure changes the entire welding condition.
The strip edges stop forging evenly. Heat concentration shifts. The V-angle becomes inconsistent. Bearings start carrying abnormal loads. Axial movement increases little by little until weld quality becomes unpredictable.
A lot of factories first suspect the HF welder.
Sometimes they replace ferrite rods.
Sometimes they adjust frequency settings again and again.
But the real problem is mechanical instability around the squeeze area.
That part is often overlooked.
Modern tube mills from MIVI Tube Machine place much more attention on squeeze rigidity, roller alignment stability, and pressure consistency because these factors directly affect weld quality during continuous production

Early Signs of Squeeze Roller Wear
The earliest symptom usually isn't catastrophic failure.
It's inconsistency.
One coil welds smoothly.
The next coil suddenly shows burr fluctuation.
Operators notice the weld bead changing shape even though the material specification hasn't changed much.
Sometimes the seam line drifts slightly left or right.
Sometimes the tube exits the welding section with visible vibration marks.
Another common sign is abnormal sound from the squeeze assembly.
Not loud at first.
More like intermittent bearing noise.
Then temperature rises around the bearing housing.
Lubrication starts burning faster.
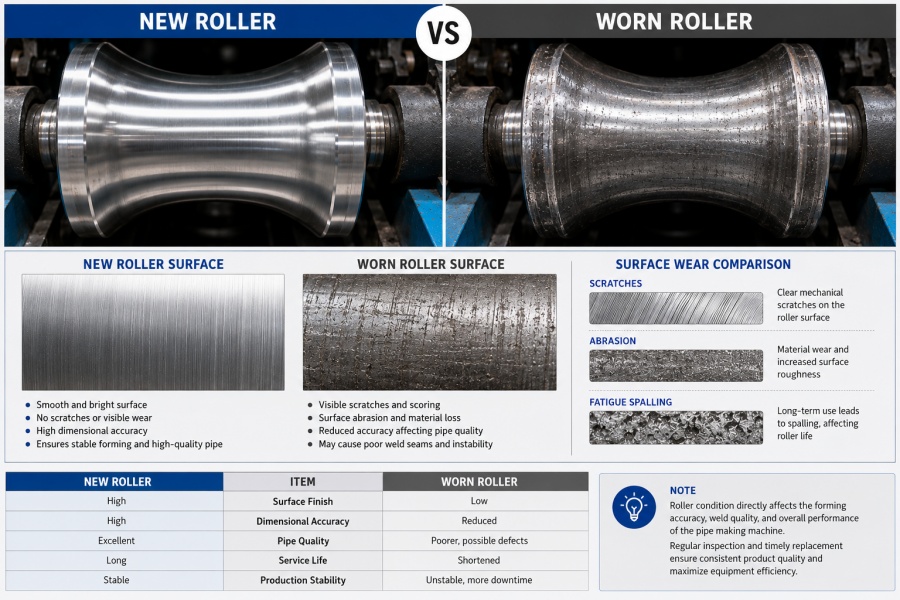
Eventually the roller surface develops uneven wear marks.
At this stage, unstable pressure becomes unavoidable.
The squeeze force no longer stays centered on the strip edges.
That directly affects forging quality during high-frequency welding.
And once pressure becomes unstable, weld consistency disappears with it.
Factories producing thin-wall tubes usually notice this earlier because thinner material reacts faster to pressure fluctuation.
High-speed production lines feel it even more.
On some older mills, axial movement becomes visible during operation.
The roller shaft shifts slightly during rotation.
Not enough to stop the machine immediately.
Enough to slowly ruin welding stability.

Why Bearing Damage Causes Unstable Welding
Inside many tube mills, squeeze roller bearings work under continuous heat, vibration, and heavy radial force.
Once lubrication condition drops, bearing clearance starts increasing.
The roller no longer rotates perfectly concentric.
Pressure becomes uneven.
Vibration transfers directly into the weld zone.
A damaged bearing also changes the contact condition between the roller and strip edge.
That’s where unstable forging begins.
Some factories continue production after hearing bearing noise because the line still “runs normally.”
But weld instability usually appears long before total bearing failure.

How Axial Movement Affects Weld Seam Quality
Axial movement is one of those problems operators often underestimate.
Even small shaft displacement affects squeeze alignment.
When the roller shifts left or right during operation, edge pressure changes constantly.
That means the heated strip edges no longer meet under stable force.
Weld consistency drops immediately.
Common causes include:
- worn bearing seats
- loose locking nuts
- shaft wear
- poor assembly precision
- long-term vibration fatigue
On high-speed ERW mills, this becomes more serious because vibration amplification increases with speed.
Some older machines simply lack enough structural rigidity around the squeeze frame.
That's one reason newer automated tube mills focus heavily on frame stability and precision alignment systems
Inspection Methods for ERW Weld Defects
Too much squeeze pressure destroys rollers faster.
Too little pressure creates weak welds.
Finding stable balance is harder than many factories expect.
Especially when coil quality changes frequently.
Or when roller wear has already started.
Pressure instability may come from hydraulic fluctuation.
But mechanical looseness is often the bigger reason.
Uneven roller surface wear also changes force distribution across the strip edge.
That creates inconsistent forging even when welding power remains unchanged.
Some operators keep increasing welding current to compensate.
That usually creates even more problems:
- excessive burr
- overheating
- edge burning
- shortened roller life
Testing & Inspection
A tube may look acceptable from outside while internal weld quality is already unstable.
That’s why inspection matters.
Especially after squeeze roller problems appear.
Hydro Test
Hydro testing often exposes weld instability very quickly.
Pipes produced under unstable squeeze pressure may fail under internal pressure even when surface appearance seems acceptable.
Small forging inconsistency becomes visible during pressure holding.
Leakage around the weld seam is common.

Flattening Test
Flattening tests reveal ductility problems around the weld area.
Poor squeeze stability usually creates incomplete bonding between strip edges.
During flattening, the seam may crack earlier than expected.
Factories producing structural pipes often rely heavily on this test because it reflects real weld integrity more directly.
UT Inspection
Many modern mills now integrate ultrasonic inspection systems directly into production lines.
That allows internal weld defects to be detected continuously instead of waiting for random offline inspection.
ome advanced production lines from MIVI Tube Machine already integrate online inspection systems to improve weld reliability during continuous operation.
UT inspection becomes especially useful when squeeze instability causes:
- incomplete fusion
- internal cracks
- porosity
- inconsistent penetration
Those defects are often difficult to identify visually.
How to Reduce Squeeze Roller Failure
Replacing rollers alone doesn't always solve the problem.
If the machine structure already has looseness or alignment deviation, new rollers wear again very quickly.
That's why experienced factories usually inspect the entire squeeze system together.
Not just the roller surface.

Improve Process Stability
A stable forming section reduces unnecessary stress on squeeze rollers.
That includes:
- better strip edge preparation
- stable V-angle control
- reduced vibration
- smoother strip tracking
When forming becomes stable, squeeze load also becomes more stable.
Roller life naturally improves.
Optimize Parameters
Many squeeze problems actually come from incorrect setup.
Pressure settings that are slightly too aggressive may not show immediate failure.
But bearing life shortens dramatically over time.
Proper adjustment should include:
- squeeze force
- welding speed
- HF power matching
- roller alignment
- bearing preload
Factories running multiple tube sizes should monitor these settings more carefully because different specifications create different squeeze loads.
Upgrade the Equipment Structure
Older mills often struggle with rigidity.
Especially after years of continuous operation.
Frame deformation, shaft wear, and assembly clearance slowly accumulate.
That's why newer ERW tube mills now focus much more on structural precision and automated stability control.
Machines from MIVI Tube Machine use reinforced structures, precision roller systems, and stable forming configurations designed for long production cycles and consistent weld quality.
For factories running high-speed production, that difference becomes very noticeable after long operating hours.
Recommended ERW Tube Mill Solutions
Tube mills designed with stronger squeeze rigidity usually maintain more stable welding over time.
Particularly in continuous production environments where vibration, heat, and load variation never really stop.
Modern automatic ERW production lines from MIVI Tube Machine support:
- stable squeeze alignment
- precision forming
- high-speed production
- online inspection integration
- fast roller replacement
- automated operation systems
Their production lines cover round, square, and rectangular tube manufacturing across multiple pipe sizes and thickness ranges.
For factories trying to reduce weld defects and maintenance downtime, squeeze stability is no longer just a mechanical detail.
It affects the entire production result.

Recommended ERW Tube Mill Solutions
Squeeze roller wear rarely appears as one single dramatic failure.
It builds slowly.
Bearing clearance increases.
Axial movement becomes larger.
Pressure stability disappears little by little.
Eventually the weld seam starts telling the story.
Factories that solve these problems early usually spend less on maintenance, produce more stable welds, and avoid unnecessary downtime later.
And in ERW tube production, stable welding almost always begins with stable squeeze pressure.
-
1. What causes squeeze roller wear in tube mills?
-
2.How does squeeze roller wear affect weld quality?
-
3. What are the signs of squeeze roller bearing damage?
-
4. How can tube mills reduce squeeze roller failure?
Regular bearing inspection, proper alignment, stable squeeze pressure, and improved machine rigidity help reduce squeeze roller wear and improve welding stability. -