


 Tube Mill Consumables: Inspection & Replacement Guide




How to Fix Weak Weld Seam in Tube Mill: The Ultimate Troubleshooting Guide
Tired of weak weld seams splitting your pipes? Learn how to tackle insufficient fusion and optimize your Mivi steel pipe making machine for high-strength, flawless welds.
Every mill manager has been there—the line seems to be humming along perfectly at 60 meters per minute, but the moment those tubes hit the sizing section or downstream bending, the seams start splitting open like a fresh zipper. It is incredibly frustrating because a weak weld seam doesn't just waste raw coils; it kills your production yield, creates massive scrap piles, and honestly, wrecks your reputation with clients who demand structural or pressure-rated piping. If your current mill is throwing these defects, you don't necessarily have a ghost in the machine. Most of the time, the culprit is hiding right inside a misaligned V-angle, a sluggish high-frequency induction setup, or a mechanical roll stand that simply cannot hold its ground anymore. Let’s look at what is actually causing these fusion failures and how you can tune your steel pipe making machine to get those flawless, clean forge lines.
What a Weak Weld Actually Looks Like on the Floor
You usually catch a weak weld in one of three ways during a live shift. First is the classic "zipper effect" where the two strip edges touch but never actually bond, causing the tube to peel apart under minimal mechanical stress with a perfectly smooth, un-fused face. Other times, you might not notice anything at the welding cross until the tube hits the sizing rolls, where the sudden external pressure forces micro-cracks to propagate along the seam. If you look closely at the weld bead before the scarfer takes it off, you might also spot dark, trapped oxide lines running continuously down the pipe—a dead giveaway that the impurities weren't squeezed out properly during the weld phase.

The Real Culprits Behind Poor Fusion
Achieving a true forged weld via high-frequency induction is all about balancing heat, speed, and physical force, and when your seams come out brittle, one of these three elements has drifted out of tolerance.
More often than not, you are dealing with straight-up insufficient fusion. If your high-frequency welder isn't pushing enough kW into the material, or if your line speed is running too fast for the current heat setting, the strip edges only reach a pasty, semi-molten state instead of a true liquidus weld temperature. They get pushed together, sure, but they don't actually knit at a molecular level.
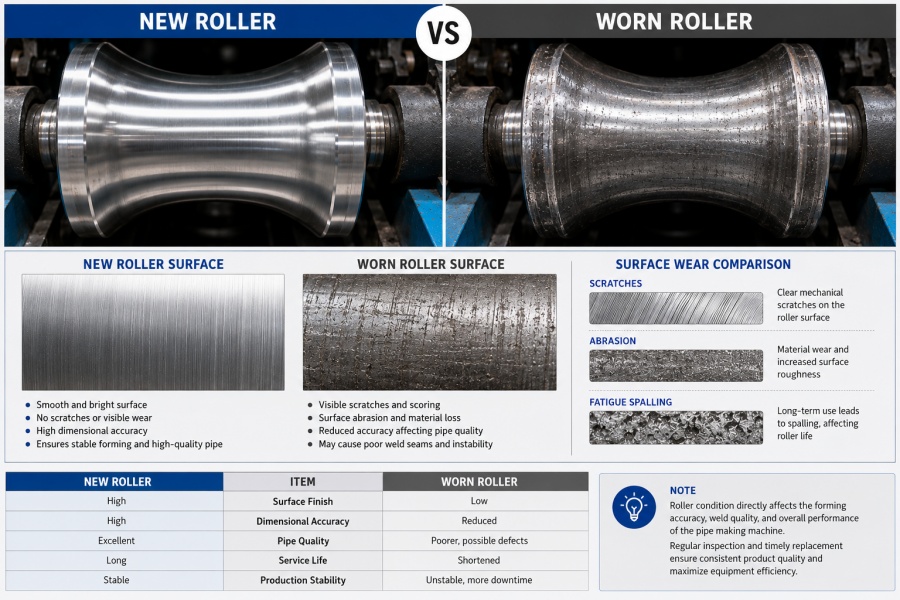
Then you have the mechanical side of things, specifically poor upset force. Even if you heat those steel edges to a perfect 1350°C, you still need enough concentrated squeezing pressure to forge them into a single piece. If your squeeze roll bearings are worn out, or if the roll tooling has worn down over millions of meters, the mill fails to generate the force required to expel the molten metal and surface oxides, leaving a weak, contaminated joint inside the tube wall.
Lastly, don't overlook unstable HF welding behavior. If your impeder is positioned too far back from the squeeze centerline, or if your cooling water pressure is surging and dipping, the induction concentration shifts constantly, creating intermittent cold spots that look fine on the outside but fail under any real pressure.

Destructive Testing to Catch the Defect Early
You cannot rely on visual inspection alone to guarantee a solid weld, which is why a rigorous testing loop is non-negotiable on a modern pipe line.
-
The Flattening Test: This is your fastest, most brutal check on the shop floor. You chop off a sample ring, place the weld at 90 degrees or 120 degrees to the direction of force, and crush it flat. If the seam splits before the walls touch, your fusion is defective.
-
Hydrostatic Pressure Testing: For fluid transmission or structural tubes that need to hold weight, running a hydro test is the ultimate insurance policy. Filling the pipe with water and cranking up the PSI exposes any pinholes or weak bonds instantly.
-
Continuous UT Inspection: Integrating an online ultrasonic testing system allows you to scan 100% of the seam in real-time, catching internal porosity or micro-fissures the moment they pass the scarfer so you don't run thousands of meters of bad product.
Engineering the Solution: Upgrading Your Process Control
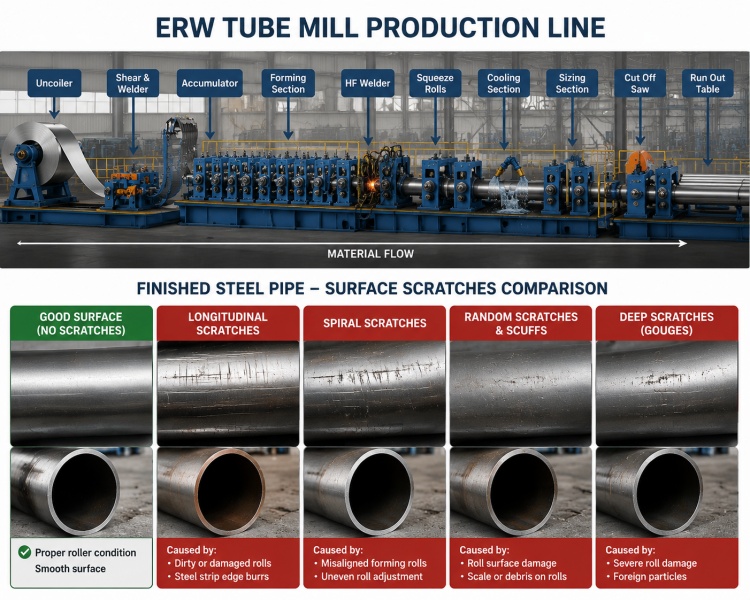
Fixing a weak seam means moving away from trial-and-error adjustments and locking down your mechanical alignment. Start with your strip edge preparation; if your breakdown and fin-pass sections aren't delivering a perfectly parallel edge into the welding guide, you will get a mismatched V-angle that causes uneven heating.
Next, check your induction geometry. Your impeder should be tucked as close to the inside diameter of the tube as possible and should extend slightly past the center of the squeeze rolls to maximize energy efficiency. If your current roll stands are flexing under heavy loads, it might be time to move away from old-style manual setups and invest in rigid, chuck-type squeeze boxes that lock the rolls into place and maintain constant upset pressure throughout the entire production run.
High-Performance Mill Spotlight: Mivi Steel Pipe Making Machine
If you are fighting loose tolerances and constant parameter drift on an aging mill, upgrading your core infrastructure is often the most cost-effective way forward.
The heavy-duty Steel Pipe Making Machine series manufactured by Mivi Machinery is engineered explicitly around weld seam stability. Built with high-rigidity cage forming technology and automated HF synchronization systems, these mills dynamically match your welding power to your exact line speed. By pairing this precise heat control with Mivi’s robust, zero-flex squeeze roll boxes, the system ensures consistent upset force across everything from thin-wall structural tubes to heavy industrial pipes, virtually eliminating the risk of insufficient fusion even during high-speed shifts.

Wrapping Up
A weak weld seam is a quick way to burn through your raw material budget and lose client trust, but it is almost always tracking back to manageable parameters like heat input and mechanical squeeze force. Keeping a close eye on your V-angle alignment and backing it up with regular flattening tests will keep your lines running clean.
If you are looking to step up your tube quality or need to troubleshoot a stubborn welding issue on your current line, check out the engineering layouts over at Mivi machinery