


 Tube Mill Consumables: Inspection & Replacement Guide



How to Improve HF Welding Quality in Tube Mills? The Complete Engineering Guide (2026)
If you want to improve HF welding quality in a tube mill, focus on seven key factors:
- Stable strip edge preparation
- Correct V-angle
- Proper HF welding power
- Balanced squeeze force
- Good ferrite rod condition
- Stable line speed
- Effective weld cooling
Most weld defects are caused by parameter imbalance rather than insufficient power. A stable welding process requires every stage of the tube mill to work together.

Key Takeaways
| Critical Factor | Importance | Typical Impact |
|---|---|---|
| Strip Edge Quality | ★★★★★ | Determines edge fusion consistency |
| V-Angle Control | ★★★★★ | Controls heat concentration |
| HF Welding Power | ★★★★★ | Provides sufficient edge heating |
| Squeeze Force | ★★★★★ | Produces solid-state forge weld |
| Ferrite Rod Condition | ★★★★☆ | Improves magnetic flux efficiency |
| Line Speed Stability | ★★★★☆ | Maintains consistent heat input |
| Cooling System | ★★★★☆ | Controls weld microstructure |
| Forming Accuracy | ★★★★★ | Ensures proper edge alignment |
In today's highly competitive steel pipe industry, weld quality has become one of the most important indicators of a tube mill's overall performance. Whether producing structural tubing, furniture tubes, automotive components, or construction pipes, manufacturers expect every weld seam to withstand flattening tests, hydrostatic pressure tests, and long-term service without failure.
However, many production managers mistakenly believe that increasing HF welder power alone will solve welding problems. In reality, HF welding is a complete manufacturing system rather than a single operation. Every section of the production line—from strip entry and forming rolls to the induction coil, squeeze rolls, cooling system, and sizing section—directly influences the final weld quality.
High-frequency induction welding is a solid-state process in which electrical current is concentrated along the strip edges as they approach the weld apex. The heated edges are then forged together under squeeze-roll pressure, expelling oxides and contaminants while creating a continuous metallurgical bond. Typical included V-angles for steel are around 2–5°, though the optimal setting depends on tube size, material, and mill configuration.
Because the process depends on precise coordination of multiple variables, even small deviations can create defects such as:
- Open seams
- Cold welds
- Burn-through
- Porosity
- Excessive weld flash
- Edge cracking
- Weld-centerline defects
- Poor flattening test performance
Instead of treating these symptoms individually, successful manufacturers adopt a systematic troubleshooting approach that evaluates the complete welding process.
nteractive HF Welding Troubleshooting Table
One of the fastest ways to diagnose weld problems is to identify the visible defect first and then trace it back to the most likely process variable.
| Production Symptom | Possible Cause | Recommended Action |
|---|---|---|
| Open seam | Insufficient squeeze force | Increase squeeze pressure and verify roll alignment |
| Cold weld | Low heat input | Increase HF power or reduce line speed |
| Burn-through | Excessive heat input | Reduce HF power or increase production speed |
| Edge cracking | Poor strip edge condition | Inspect strip quality and edge preparation |
| Porosity | Dirty or oxidized strip edges | Remove oil, rust, and contaminants before welding |
| Excessive flash | Over-squeezing | Reduce squeeze force and confirm proper V-angle |
| Unstable weld seam | Incorrect induction coil position | Adjust coil-to-apex distance and alignment |
| Frequent weld failure | Multiple process imbalance | Review forming, welding, cooling, and sizing together |
This diagnostic approach is more effective than changing welding parameters randomly because most weld failures result from the interaction of several process variables rather than a single equipment fault.
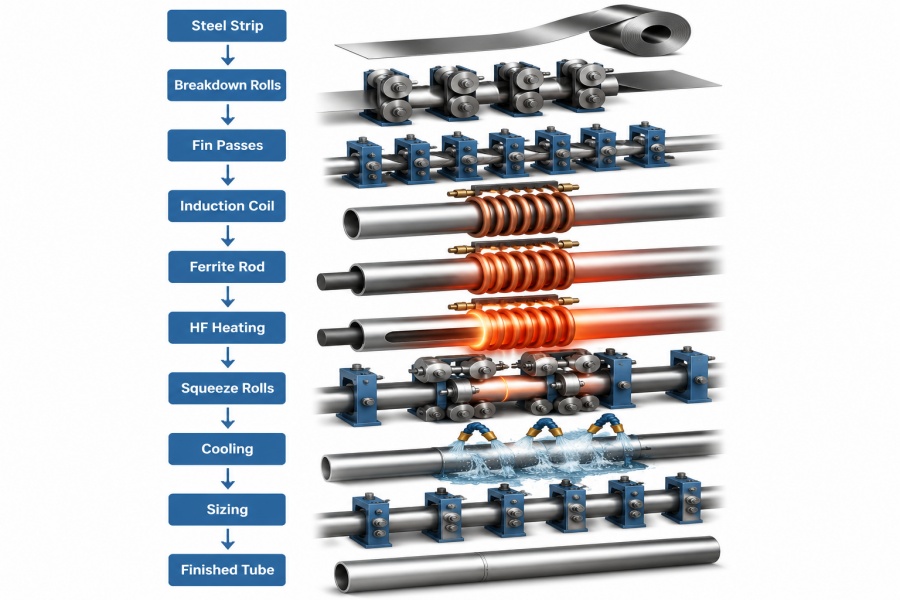
What Determines HF Welding Quality?
Many engineers ask a simple question:
What is the single most important factor affecting HF welding quality?
The answer is there is no single factor.
HF welding quality is determined by the balance of several interrelated variables. Improving only one parameter—such as increasing welding power—rarely eliminates defects if strip presentation, V-angle, or squeeze force remain incorrect. Experienced tube mill operators therefore treat the welding section as an integrated process rather than a collection of independent machines.
The primary factors influencing weld quality include:
1. Steel Strip Quality
The strip must have:
- Uniform thickness
- Clean edges
- Minimal burrs
- Stable chemical composition
- Consistent mechanical properties
Even advanced HF welding equipment cannot compensate for poor incoming strip quality. Variations in edge condition or material consistency often lead to unstable heating and weak weld seams.
2. Forming Section Accuracy
Before welding begins, the strip must be formed into a precise tubular shape.
Poor forming can result in:
- Uneven edge presentation
- Edge mismatch
- Unstable V-angle
- Strip wandering
- Excessive springback
These issues reduce current concentration at the weld apex and increase the likelihood of incomplete fusion.
3. V-Angle Geometry
The V-angle determines how electrical current is concentrated at the strip edges before forging.
If the V-angle is too large:
- Heat becomes dispersed.
- Welding efficiency decreases.
- Power consumption increases.
If the V-angle is too small:
- Premature arcing may occur.
- Heat distribution becomes unstable.
- Weld consistency deteriorates.
Maintaining a stable V-angle is therefore essential for achieving consistent weld quality.

4. Squeeze Force
The squeeze rolls do more than press the tube closed. Their primary function is to forge the heated strip edges together while expelling molten oxides and impurities.
Incorrect squeeze force may produce:
- Weak metallurgical bonding
- Excessive weld flash
- Wall-thickness reduction
- Dimensional inaccuracies
Proper adjustment ensures a sound solid-state weld with consistent mechanical properties.
5. Induction Coil and Ferrite Performance
The induction coil delivers high-frequency energy, while the ferrite rod concentrates the magnetic field toward the weld V.
A damaged ferrite rod or poorly positioned induction coil can reduce heating efficiency, increase power consumption, and create unstable weld temperatures. Routine inspection of these components helps maintain process consistency.
6. Cooling and Sizing
After welding, controlled cooling stabilizes the weld microstructure before the tube enters the sizing section.
Improper cooling can lead to:
- Residual stress
- Distortion
- Reduced mechanical properties
- Dimensional instability
The sizing section then restores the tube to its specified dimensions without overstressing the freshly welded seam.
One of the most overlooked factors in HF welding is the quality of the steel strip edge. Operators often focus on adjusting welding power, squeeze pressure, or line speed, while ignoring the condition of the strip entering the mill. In reality, the welding process begins long before the induction coil. If the strip edges are damaged, contaminated, or poorly slit, even the most advanced HF welder cannot consistently produce a sound weld. Proper fin-pass design and strip preparation are specifically intended to present clean, parallel edges to the welding section.
6. Cooling and Sizing
After welding, controlled cooling stabilizes the weld microstructure before the tube enters the sizing section.
Improper cooling can lead to:
- Residual stress
- Distortion
- Reduced mechanical properties
- Dimensional instability
The sizing section then restores the tube to its specified dimensions without overstressing the freshly welded seam.

Keep Strip Edges Clean and Uniform
One of the most overlooked factors in HF welding is the quality of the steel strip edge. Operators often focus on adjusting welding power, squeeze pressure, or line speed, while ignoring the condition of the strip entering the mill. In reality, the welding process begins long before the induction coil. If the strip edges are damaged, contaminated, or poorly slit, even the most advanced HF welder cannot consistently produce a sound weld. Proper fin-pass design and strip preparation are specifically intended to present clean, parallel edges to the welding section.
Why Strip Edge Quality Matters
HF current naturally follows the path of least electrical resistance and becomes concentrated along the strip edges because of the skin and proximity effects. When both edges are smooth, parallel, and uniform, heating remains balanced and the squeeze rolls can create a strong forge weld.
However, damaged edges disturb current flow and heat distribution, leading to unstable welding conditions.
Typical edge defects include:
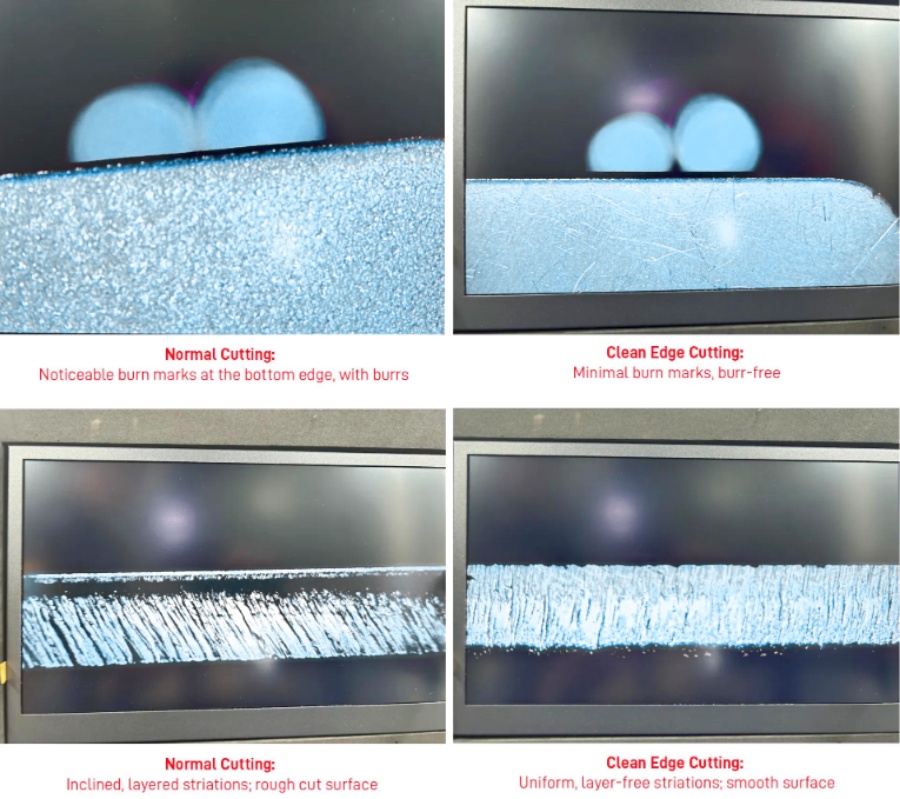
- Burrs after slitting
- Rust or scale
- Oil contamination
- Edge waviness
- Edge dents
- Scratches
- Slivers
- Edge mismatch
Each of these defects changes how current travels through the V-zone and may cause localized overheating or insufficient fusion.
Common Strip Edge Problems
| Strip Edge Condition | Influence on Welding | Recommended Action |
|---|---|---|
| Burr | Pre-arcing, unstable current | Improve slitting quality |
| Rust | Poor electrical contact | Remove before production |
| Oil | Porosity | Clean strip surface |
| Wavy edge | Unstable V-angle | Correct forming |
| Edge dent | Poor edge alignment | Reject damaged coil |
| Sliver | Oxide inclusion | Improve slitting process |
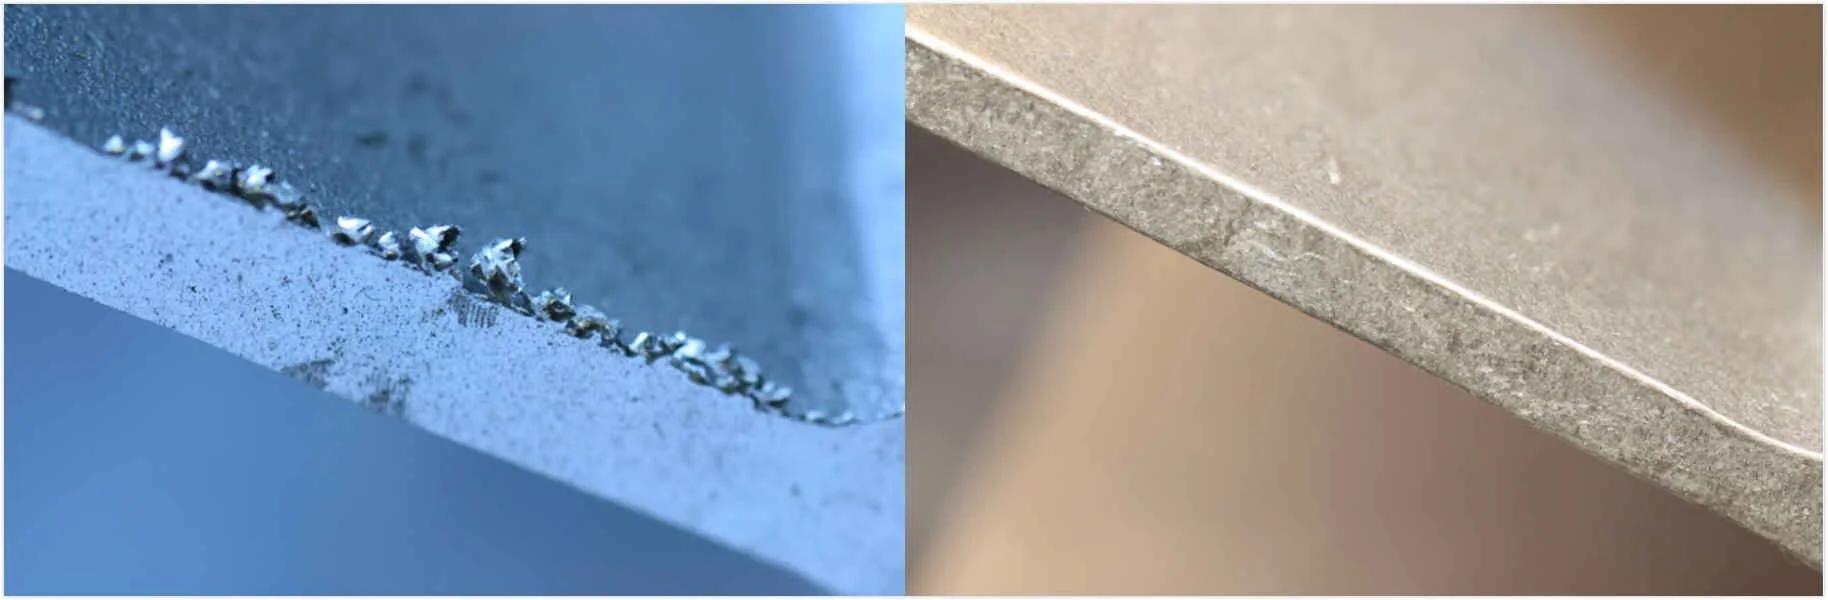
Burrs Are More Dangerous Than Many Operators Realize
A burr only a few tenths of a millimeter high can significantly change the way strip edges meet.
Instead of making full contact simultaneously, one side touches first.
This causes:
- Premature current concentration
- Local overheating
- Pre-arcing
- Oxide entrapment
- Weak weld bond
Eventually these defects may appear as:
- Flattening test cracks
- Hydrostatic leakage
- Ultrasonic indications
- Weld seam opening
Industry guidance recommends maintaining smooth slit edges because burrs and roughness inhibit consistent weld formation.
Steel Chemistry Also Affects Weld Quality
Although operators cannot change steel chemistry during production, they should understand its influence.
Variations in:
- Carbon
- Manganese
- Silicon
- Phosphorus
- Sulfur
change:
- Heating characteristics
- Plastic deformation
- Oxide formation
- Forge welding behavior
For this reason, changing coil suppliers sometimes requires adjustments to welding power or squeeze settings.
Practical Inspection Checklist
Before every production shift, inspect:
✓ Strip width consistency
✓ Strip thickness
✓ Burr height
✓ Rust
✓ Oil contamination
✓ Coil camber
✓ Edge damage
✓ Surface scratches
Five minutes of inspection can prevent hours of downtime later.
Optimize the V-Angle
Among all welding parameters, the V-angle is probably the most misunderstood.
Many operators try to increase welding power when defects appear.
Experienced engineers usually inspect the V-angle first.
The V-angle is the included angle formed by the approaching strip edges immediately before they enter the squeeze rolls. It determines where the high-frequency current is concentrated and where heating occurs. Typical included angles for carbon-steel HF welding are around 2–5° (many production mills operate in the 3–6° range depending on tube size and tooling).
Factors That Influence the V-Angle
The V-angle is affected by more than guide roll adjustment.
It is also influenced by:
- Forming accuracy
- Fin pass design
- Guide roll position
- Strip thickness
- Coil width tolerance
- Strip springback
- Distance from last fin pass to squeeze rolls
This is why experienced tube mill technicians always inspect the forming section before changing welding parameters.
Recommended V-Angle Troubleshooting
| Observation | Possible Cause | Suggested Action |
|---|---|---|
| V-angle wider than normal | Guide rolls moved | Readjust guides |
| V-angle unstable | Poor forming | Inspect fin passes |
| Frequent pre-arcing | Opening too small | Increase V-angle slightly |
| Cold weld | Opening too large | Reduce V-angle |
| Roll pickup | Premature edge contact | Recheck fin tooling |
Practical Production Tips
Experienced mill operators generally follow these principles:
- Keep the last fin pass as close as practical to the weld rolls.
- Maintain symmetrical edge presentation.
- Avoid strip wandering.
- Monitor V-angle whenever changing strip thickness.
- Recheck guide rolls after every tooling change.
- Verify induction coil alignment after maintenance.
Small adjustments made early often prevent expensive downstream defects.
Practical Production Tips
Experienced mill operators generally follow these principles:
- Keep the last fin pass as close as practical to the weld rolls.
- Maintain symmetrical edge presentation.
- Avoid strip wandering.
- Monitor V-angle whenever changing strip thickness.
- Recheck guide rolls after every tooling change.
- Verify induction coil alignment after maintenance.
Small adjustments made early often prevent expensive downstream defects.

Balance HF Welding Power and Line Speed
If there is one adjustment that operators make more often than any other, it is increasing welding power. Whenever a weld appears weak or a flattening test fails, the first reaction is frequently to raise the HF power setting.
Unfortunately, this approach often treats the symptom rather than the cause.
HF welding quality depends on the relationship between heat input and production speed, not on power alone. The key parameter is the amount of energy delivered to each meter of strip. If line speed changes without a corresponding adjustment in power, the weld temperature and metallurgical structure also change. Studies have shown that the ratio between welding power and line speed (heat input factor), together with squeeze force, has a major influence on tensile strength, toughness, hardness, and weld integrity.
Why Heat Input Matters
Heat input determines whether the strip edges reach the proper forging temperature before entering the squeeze rolls.
Too little heat results in incomplete bonding.
Too much heat causes excessive melting, unstable flash, and unnecessary energy consumption.
The objective is not maximum temperature, but the correct temperature at the correct production speed.
Typical Symptoms
| Symptom | Likely Cause | Recommended Adjustment |
|---|---|---|
| Cold weld | Heat input too low | Increase power or reduce speed |
| Burn-through | Heat input too high | Reduce power or increase speed |
| Heavy flash | Excessive heat | Reduce power and verify squeeze |
| Weak weld | Heat and squeeze imbalance | Optimize both together |
| High power consumption | Incorrect inductor position | Check coil placement |
Common Mistake
Many factories slow down production when welding becomes unstable.
Sometimes this helps.
Sometimes it makes the weld even hotter.
A better method is to evaluate:
- Line speed
- HF power
- V-angle
- Squeeze force
- Induction coil position
as one integrated system rather than changing only one parameter. Research consistently shows that welding quality improves when these variables are optimized together rather than independently.
Balance HF Welding Power and Line Speed
If there is one adjustment that operators make more often than any other, it is increasing welding power. Whenever a weld appears weak or a flattening test fails, the first reaction is frequently to raise the HF power setting.
Unfortunately, this approach often treats the symptom rather than the cause.
HF welding quality depends on the relationship between heat input and production speed, not on power alone. The key parameter is the amount of energy delivered to each meter of strip. If line speed changes without a corresponding adjustment in power, the weld temperature and metallurgical structure also change. Studies have shown that the ratio between welding power and line speed (heat input factor), together with squeeze force, has a major influence on tensile strength, toughness, hardness, and weld integrity.
Why Heat Input Matters
Heat input determines whether the strip edges reach the proper forging temperature before entering the squeeze rolls.
Too little heat results in incomplete bonding.
Too much heat causes excessive melting, unstable flash, and unnecessary energy consumption.
The objective is not maximum temperature, but the correct temperature at the correct production speed.
| Symptom | Likely Cause | Recommended Adjustment |
|---|---|---|
| Cold weld | Heat input too low | Increase power or reduce speed |
| Burn-through | Heat input too high | Reduce power or increase speed |
| Heavy flash | Excessive heat | Reduce power and verify squeeze |
| Weak weld | Heat and squeeze imbalance | Optimize both together |
| High power consumption | Incorrect inductor position | Check coil placement |
Common Mistake
Many factories slow down production when welding becomes unstable.
Sometimes this helps.
Sometimes it makes the weld even hotter.
A better method is to evaluate:
- Line speed
- HF power
- V-angle
- Squeeze force
- Induction coil position
as one integrated system rather than changing only one parameter. Research consistently shows that welding quality improves when these variables are optimized together rather than independently.
Adjust Squeeze Force Correctly
Many people assume the squeeze rolls simply close the tube.
In fact, they perform one of the most important functions in the entire welding process.
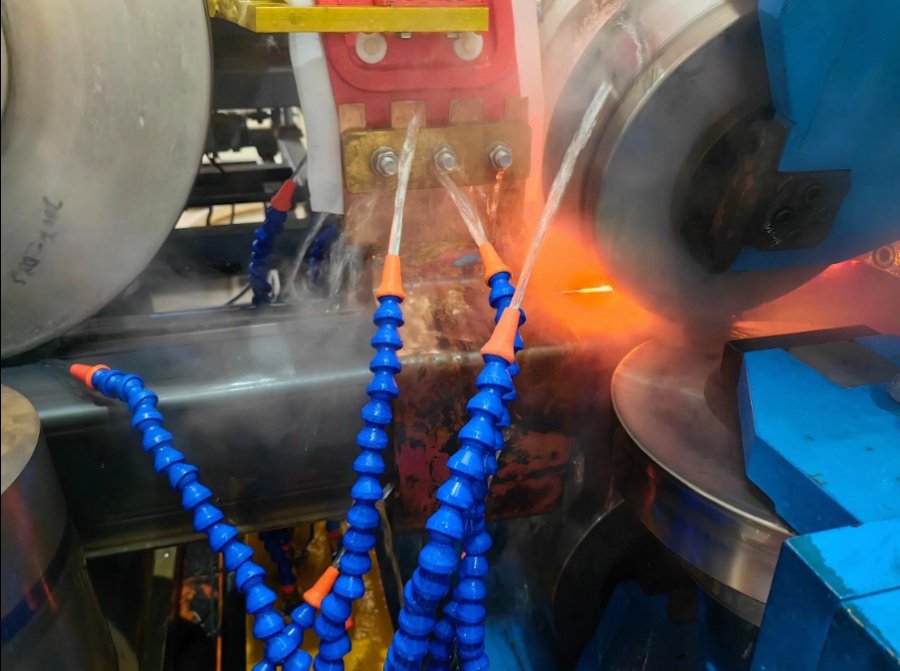
The squeeze rolls forge the heated strip edges together while forcing molten oxides and contaminants out of the weld zone.
Without sufficient upset pressure, even perfectly heated strip edges cannot produce a sound weld.
Conversely, excessive squeeze creates unnecessary flash, wall reduction, and dimensional instability. Research and industrial practice both indicate that weld quality is controlled by the balance between heat input and squeeze force—not by either parameter alone.
What Happens with Too Little Squeeze?
Insufficient squeeze may produce:
- Open seams
- Cold welds
- Oxide inclusions
- Weak metallurgical bonding
- Poor flattening performance
These defects may not be visible immediately but often appear during hydrostatic testing or in service.
What Happens with Too Much Squeeze?
Excessive pressure can cause:
- Large external flash
- Internal flash growth
- Wall thinning
- Pipe deformation
- Increased roll wear
- Higher operating costs
The objective is to apply enough upset force to expel impurities without deforming the tube.
Practical Adjustment Tips
Experienced operators normally:
- Observe flash symmetry.
- Check weld centerline appearance.
- Monitor flattening test results.
- Verify wall thickness.
- Compare current consumption before and after adjustments.
Small changes usually produce better results than large corrections.
Troubleshooting Table
| Observation | Possible Cause | Solution |
|---|---|---|
| Open seam | Low squeeze | Increase pressure |
| Large flash | Over squeeze | Reduce pressure |
| Thin wall | Excessive upset | Readjust roll gap |
| Weak weld | Poor upset | Optimize squeeze and heat together |

Adjust Squeeze Force Correctly
Ferrite rods (impeders) are among the least expensive consumables in an HF welding system, yet they have a major influence on welding efficiency.
Their purpose is to concentrate the magnetic field inside the tube so that more electrical energy reaches the strip edges instead of being lost around the tube circumference.
When ferrite performance declines, operators often compensate by increasing welding power—raising electricity consumption without solving the root cause. Ferrite material, geometry, cooling, and positioning all affect current concentration and overall welding efficiency.
What Happens with Too Little Squeeze?
Insufficient squeeze may produce:
- Open seams
- Cold welds
- Oxide inclusions
- Weak metallurgical bonding
- Poor flattening performance
These defects may not be visible immediately but often appear during hydrostatic testing or in service.
What Happens with Too Much Squeeze?
Excessive pressure can cause:
- Large external flash
- Internal flash growth
- Wall thinning
- Pipe deformation
- Increased roll wear
- Higher operating costs
The objective is to apply enough upset force to expel impurities without deforming the tube.
Practical Adjustment Tips
Experienced operators normally:
- Observe flash symmetry.
- Check weld centerline appearance.
- Monitor flattening test results.
- Verify wall thickness.
- Compare current consumption before and after adjustments.
Small changes usually produce better results than large corrections.
Troubleshooting Table
| Observation | Possible Cause | Solution |
|---|---|---|
| Open seam | Low squeeze | Increase pressure |
| Large flash | Over squeeze | Reduce pressure |
| Thin wall | Excessive upset | Readjust roll gap |
| Weak weld | Poor upset | Optimize squeeze and heat together |
Inspect Ferrite Rods Frequently
Ferrite rods (impeders) are among the least expensive consumables in an HF welding system, yet they have a major influence on welding efficiency.
Their purpose is to concentrate the magnetic field inside the tube so that more electrical energy reaches the strip edges instead of being lost around the tube circumference.
When ferrite performance declines, operators often compensate by increasing welding power—raising electricity consumption without solving the root cause. Ferrite material, geometry, cooling, and positioning all affect current concentration and overall welding efficiency.
Signs That Ferrite Needs Inspection
- Cracked ferrite
- Worn ends
- Broken segments
- Discoloration from overheating
- Reduced welding efficiency
- Increased generator load
Correct Ferrite Position
Good positioning means:
- Close to the weld apex
- Centered within the tube
- Stable during production
- Adequately cooled
Poor positioning reduces magnetic efficiency and causes uneven heating.
Daily Inspection Checklist
✓ Ferrite length
✓ Ferrite diameter
✓ Surface cracks
✓ Cooling water flow
✓ Ferrite alignment
✓ Temperature
Routine inspection often prevents unexpected production interruptions.

Maintain Stable Line Speed
Although modern tube mills operate with PLC and servo controls, line-speed fluctuations remain a common source of inconsistent weld quality.
Every speed change alters the time available for heating.
If power remains unchanged while speed increases:
- Heat input decreases.
- Strip edges may not reach forging temperature.
If speed decreases:
- Heat input rises.
- Overheating becomes more likely.
Maintaining a stable production speed is therefore just as important as selecting the correct power level.
Causes of Speed Fluctuation
- Motor instability
- Accumulator inconsistency
- Coil-end joining
- PLC tuning issues
- Mechanical drag
Best Practices
- Avoid frequent acceleration.
- Maintain synchronized drives.
- Monitor power consumption trends.
- Review production data after each coil.
Improve Cooling Efficiency
Cooling begins immediately after the squeeze rolls.
Its purpose is not only to reduce temperature but also to stabilize the weld microstructure before sizing.
Poor cooling can produce:
- Residual stress
- Dimensional instability
- Distortion
- Reduced toughness
Cooling is equally important for ferrite rods and induction coils. Ferrite performance decreases rapidly if operating temperatures become excessive, making proper coolant flow and filtration essential.
Characteristics of an Effective Cooling System
- Uniform water distribution
- Stable pressure
- Clean filtered coolant
- Correct nozzle position
- Adequate flow around the weld seam
Cooling System Checklist
| Inspection Item | Frequency |
|---|---|
| Water pressure | Every shift |
| Nozzle blockage | Daily |
| Water temperature | Continuous |
| Filter cleanliness | Weekly |
| Coil cooling | Daily |
| Ferrite cooling | Daily |
Real Production Case: How a Small Adjustment Reduced Weld Defects by More Than 80%
One of the biggest misconceptions in HF welding is that every weld defect requires more welding power. In practice, many quality issues originate from the interaction of several process parameters rather than a lack of heat.
Case Background
A steel tube manufacturer producing 50 × 50 × 2.0 mm carbon steel tubes experienced:
- Frequent flattening test failures
- Random hydrostatic leakage
- Large external weld flash
- Increased power consumption
- Scrap rate above 6%
The maintenance team initially increased HF welding power several times.
Unfortunately, the defect rate became even worse.
Engineering Investigation
After inspecting the complete welding section, engineers identified several contributing factors:
- Excessive squeeze force
- Slightly oversized V-angle
- Worn ferrite rods
- Unstable strip edge presentation
Each issue alone appeared minor, but together they disrupted weld stability.
Corrective Actions
Instead of increasing power again, the team:
- Reduced squeeze pressure
- Re-adjusted the V-angle
- Replaced worn ferrite rods
- Corrected strip guiding
- Rebalanced welding power with line speed
Results
Within one production shift:
| KPI | Before | After |
|---|---|---|
| Scrap Rate | >6% | <1% |
| Flattening Pass Rate | Unstable | Stable |
| Weld Appearance | Variable | Consistent |
| Power Consumption | High | Reduced |
| Production Stability | Frequent Stops | Continuous |
Stable HF welding comes from balancing the entire process—not from increasing generator power.
Common HF Welding Mistakes
Even experienced operators can fall into habits that reduce weld quality.
Mistake 1: Increasing Power for Every Defect
Not every weld defect is caused by insufficient heat.
Weak welds may instead result from:
- Incorrect V-angle
- Poor strip edges
- Low squeeze force
- Ferrite deterioration
Mistake 2: Ignoring Strip Quality
Even a premium HF welder cannot compensate for:
- Heavy burrs
- Oil contamination
- Rust
- Edge mismatch
Incoming strip quality is the foundation of weld quality.
Mistake 3: Never Inspecting Ferrite Rods
Ferrite rods gradually lose efficiency through:
- Cracking
- Thermal shock
- Mechanical wear
Operators often compensate by increasing power, leading to higher energy costs instead of solving the real issue.
Mistake 4: Using Visual Inspection Only
A weld can appear smooth externally while containing:
- Oxide inclusions
- Lack of fusion
- Hook cracks
- Cold welds
Modern production should combine:
- Visual inspection
- Flattening test
- Hydrostatic test
- Eddy current or ultrasonic testing
Mistake 5: Adjusting Multiple Parameters Simultaneously
Changing:
- HF power
- Squeeze force
- Line speed
- Guide rolls
at the same time makes troubleshooting almost impossible.
A disciplined approach—changing one parameter, recording the result, and then moving to the next—helps identify the true root cause.
H2. Common HF Welding Defects and Solutions
One reason AI search engines frequently surface technical articles is the presence of concise diagnostic tables.
The following matrix summarizes the most common HF welding defects.
| Defect | Typical Cause | Recommended Solution |
|---|---|---|
| Open seam | Low squeeze force | Increase upset pressure |
| Cold weld | Insufficient heat input | Increase power or reduce speed |
| Burn-through | Excessive heat | Reduce power |
| Oxide inclusion | Dirty strip edges | Improve strip preparation |
| Hook crack | Poor V-angle or strip mismatch | Adjust forming section |
| Large flash | Excessive squeeze | Reduce squeeze force |
| Internal flash | Incorrect upset | Optimize roll gap |
| Porosity | Oil or moisture | Clean strip before welding |
| Edge crack | Poor strip quality | Improve incoming material |
| Weld offset | Strip misalignment | Correct guide rolls |
These defects are typically influenced by a combination of welding speed, squeeze force, heat input, strip alignment, and edge condition rather than a single parameter.
Recommended HF Welding Parameter Checklist
A daily parameter review helps maintain process consistency.
| Parameter | Recommended Check |
|---|---|
| Strip Width | Stable |
| Strip Thickness | Within tolerance |
| Strip Edge | Clean |
| V-angle | Consistent |
| Induction Coil | Centered |
| Ferrite Rod | Good condition |
| HF Power | Stable |
| Line Speed | Constant |
| Squeeze Force | Balanced |
| Cooling Water | Adequate |
| Finished Tube Size | Verified |
Recording these values shift by shift makes it easier to detect trends before defects become costly.
Frequently Asked Questions (FAQ)
What is the most important factor affecting HF welding quality?
There is no single factor. High-quality welds require a balanced combination of strip quality, forming accuracy, V-angle, heat input, squeeze force, ferrite condition, and cooling.
Why does my weld fail the flattening test but pass the hydro test?
Hydrostatic testing mainly checks for leakage under pressure, while the flattening test evaluates ductility and the integrity of the metallurgical bond. Hidden defects such as oxide inclusions or lack of fusion may survive hydrostatic testing but fail during flattening.
Can increasing HF power always improve weld quality?
No. Excessive heat may increase flash, distort the weld, or create brittle microstructures. Welding quality depends on balancing heat input, line speed, and squeeze force rather than maximizing power.
How often should ferrite rods be replaced?
Inspect ferrite rods daily for cracks, wear, overheating, and reduced efficiency. Replacement intervals depend on production volume, material type, and cooling conditions rather than a fixed schedule.
Why does weld quality suddenly become unstable after changing steel coils?
Different coils may vary in chemistry, edge quality, thickness tolerance, and surface condition. These differences can require adjustments to welding power, V-angle, and squeeze force to maintain consistent weld quality.
Daily Quality Inspection Checklist
□ Strip Edge
□ Roll Alignment
□ Guide Roll Position
□ V-Angle
□ HF Generator Output
□ Ferrite Rod Condition
□ Coil Position
□ Squeeze Roll Gap
□ Cooling Water
□ Weld Flash
□ Tube Diameter
□ Wall Thickness
□ Weld Appearance
□ Flattening Test
□ Hydro Test
□ UT/ECT Inspection
Conclusion
High-frequency welding is not simply a matter of supplying more electrical power. A reliable weld seam results from the coordinated performance of the entire tube mill—from strip preparation and forming to induction heating, squeeze forging, cooling, and final sizing.
Manufacturers that consistently achieve high weld quality share several practices:
- Maintain clean, uniform strip edges.
- Control the V-angle throughout production.
- Balance heat input with line speed.
- Apply the correct squeeze force.
- Inspect ferrite rods regularly.
- Keep cooling systems efficient.
- Verify weld quality through routine testing.
By treating the welding section as an integrated process instead of adjusting isolated parameters, tube producers can reduce scrap, improve mechanical performance, and lower production costs. Modern research and field experience consistently show that weld integrity depends on the interaction of heat input, squeeze force, strip condition, and process stability.、
Call to Action
Improve Your Tube Mill Welding Performance with MIVI
If your production line experiences:
- Flattening test failures
- Hydrostatic leakage
- Cold welds
- Excessive weld flash
- High scrap rates
- Unstable HF welding
our engineering team can help.
MIVI provides complete ERW tube mill solutions, including:
- HF welding process optimization
- Tube mill troubleshooting
- Ferrite rod recommendations
- Roll tooling optimization
- Production line upgrades
- Remote technical support
Contact MIVI today for a professional HF welding assessment and discover how to improve weld quality, reduce defects, and maximize production efficiency.
-
1. What is the material of the pipe that the machine produce
GI pipe, Steel pipe, Mild steel pipe, Low carbon steel pipe -
2. Is it possible to customize the equipment according to the demanding of the customer?
-
3. Do you have any certificates?
-
4. What is the payment method?
-
5. What does the after-service do you provide?
-
6. When will the engineer arrive?
-
7. How long will the installation and staff training?
-
8. Do you have reference project?
-
9. What about spare parts?