


 Tube Mill Consumables: Inspection & Replacement Guide

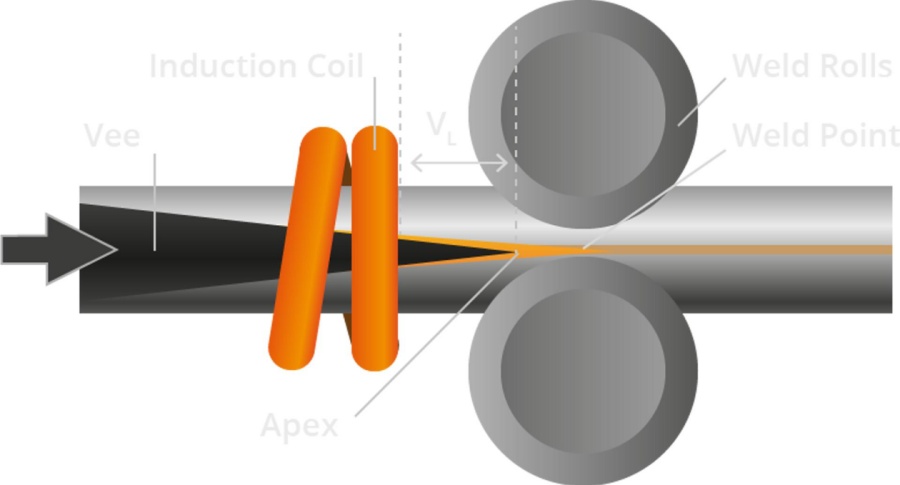


How to Prevent Tube Mill Rolls from Rusting During Machine Shutdown?
Rust prevention is important because corrosion on the working surface of a forming roll can create surface marks, affect roll geometry and increase the risk of unstable tube forming after restart. Therefore, tube mill roller maintenance should begin before the machine is left idle—not when rust has already appeared.
A tube mill may be shut down for a few days, a planned holiday, maintenance work, or even several months. What happens to the forming rolls during that time is easy to overlook. The machine is not running, so there is no obvious production problem. But when the line is started again, operators may suddenly find rust spots on the roll surface, marks on the tube, or a roll that no longer looks the way it did before the shutdown.
Coolant left around the roll grooves, moisture in the workshop, steel particles from production, and temperature changes can all create conditions for corrosion. Leaving a set of tube mill rollers exposed for an extended period is therefore not a good storage method, even if the rolls were working normally when production stopped.
For most tube mills, the basic maintenance principle is straightforward: clean the rolls after production, make sure the surfaces are completely dry, protect the exposed metal, and store the tooling somewhere dry and clean. The longer the shutdown, the more attention should be given to packaging and moisture control.
Why Can Tube Mill Rolls Rust During a Shutdown?
During production, the roll surface of an ERW tube mill is constantly exposed to coolant, steel particles, dust and the surrounding workshop environment.Once the mill stops, however, the situation changes..
A small amount of moisture trapped in a roll groove may remain there for days. In a humid workshop, condensation can make the situation worse, especially when the temperature changes between day and night. Coastal factories and plants with poor ventilation usually need to pay even more attention to this.
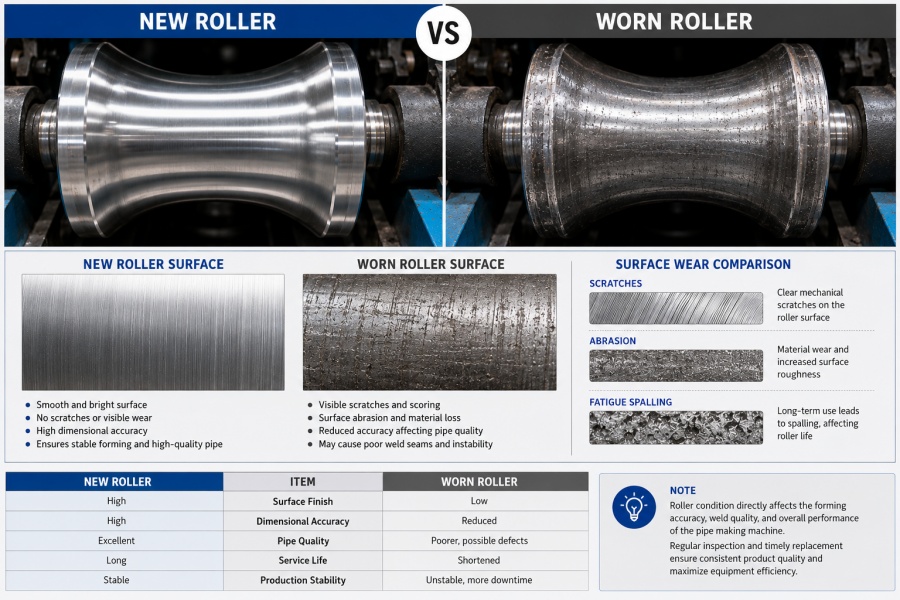
The working surface of a forming roll is not an area where corrosion should be taken lightly. A small rust mark may look harmless, but deeper corrosion can create pits or alter the surface condition of the roll. After restarting the mill, those imperfections can contribute to roll marks or surface defects on the finished tube.
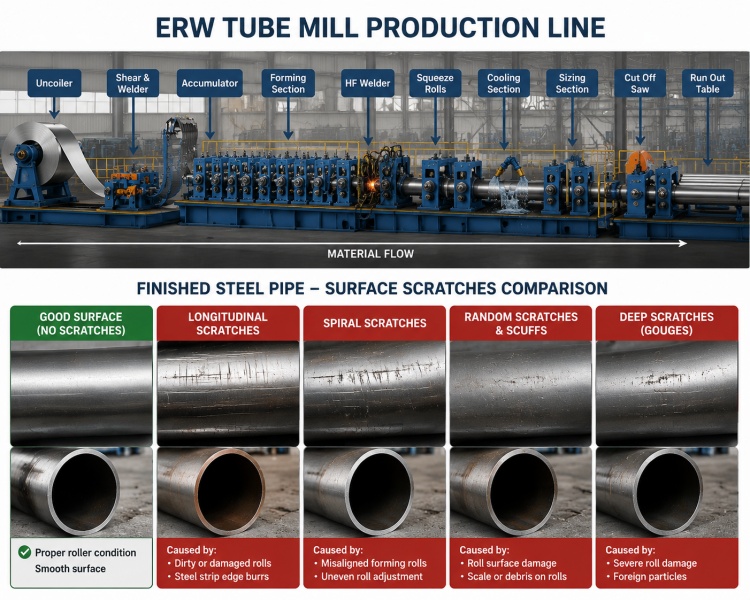
MIVI's tube mill equipment is designed around a continuous forming, welding, cooling and sizing process, so the condition of the tooling directly matters to the stability of the production line.
That is why a shutdown should be treated as part of the roll maintenance cycle, rather than simply a period when the machine is not operating.
What Should Be Done Before Storing Tube Mill Rollers?
The first thing to do is not apply oil. It is to clean the roll.
This sounds obvious, but it is one of the steps that is most easily skipped when production stops late in a shift. If coolant, steel dust or moisture remains on the working surface, applying a protective coating over it does not solve the underlying problem.
The rolls should be inspected while they are being cleaned. Look closely at the grooves and other areas where material tends to accumulate. Remove steel particles and production residue, wipe away coolant and oil contamination, and use a clean cloth to dry the surfaces.
There is also a good opportunity here to record the condition of the tooling.
If a roll already has abnormal wear, scratches or small corrosion marks, take photographs and note the condition before putting it into storage. This makes the next inspection much easier and can help determine whether the problem existed before the shutdown.
MIVI's guide to tube mill maintenance also emphasizes monitoring roll wear rather than waiting until poor tube dimensions or surface quality force a replacement.
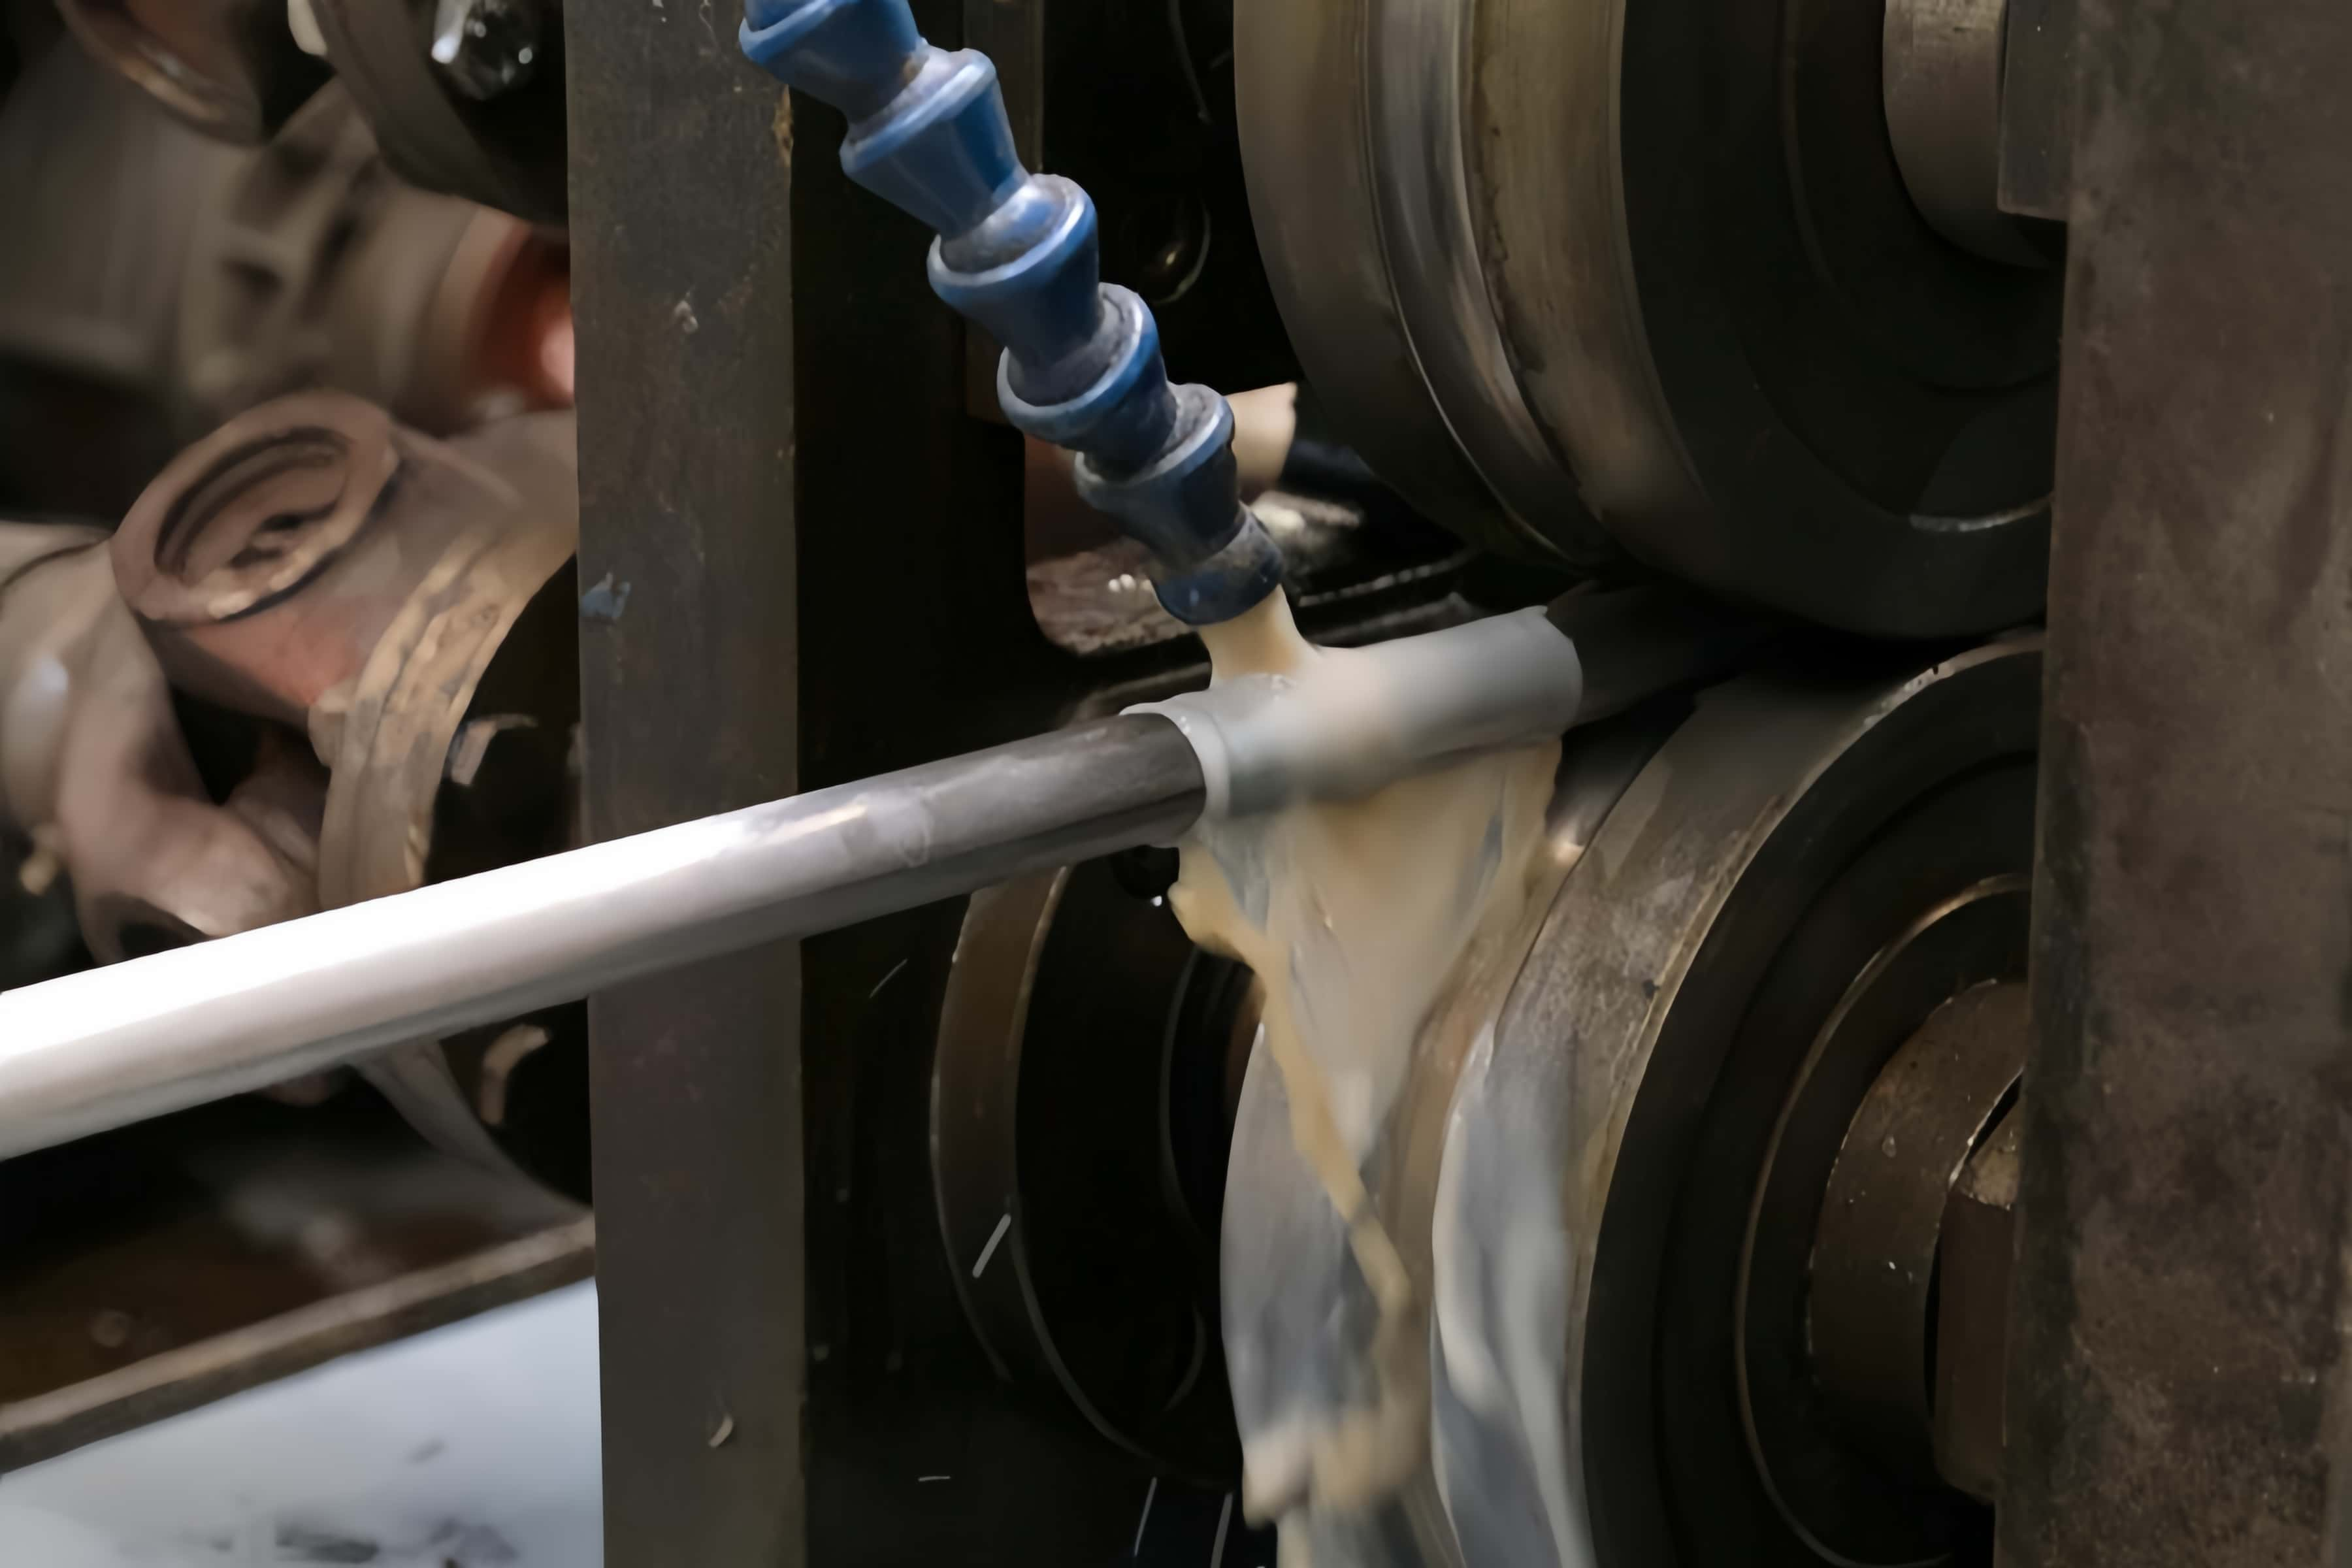
Should Anti-Rust Oil Be Applied to Tube Mill Rolls?
In most cases, yes, but the type and amount of protection should match the storage conditions.
A thin, even protective film can help prevent moisture from reaching an exposed steel surface. The important point is coverage. Pay attention to the roll grooves, edges, shaft areas and other exposed metal surfaces rather than only coating the easiest areas to reach.
There is also no reason to assume that more oil always means better protection. Excessive oil can collect dust and make the rolls unpleasant to handle later. The coating should be appropriate for the expected storage period and the manufacturer's recommendations should be followed.
For a short shutdown, such as a weekend or a few days, cleaning, drying and a suitable corrosion inhibitor may be enough. A machine that will remain idle for several months deserves more protection, particularly if the factory is humid.
For longer storage, VCI paper or film, sealed protective packaging and moisture-control measures can be considered in addition to the corrosion-preventive coating.
The objective is not to create a thick layer of oil. It is to keep moisture away from the metal surface for as long as the tooling remains out of service.
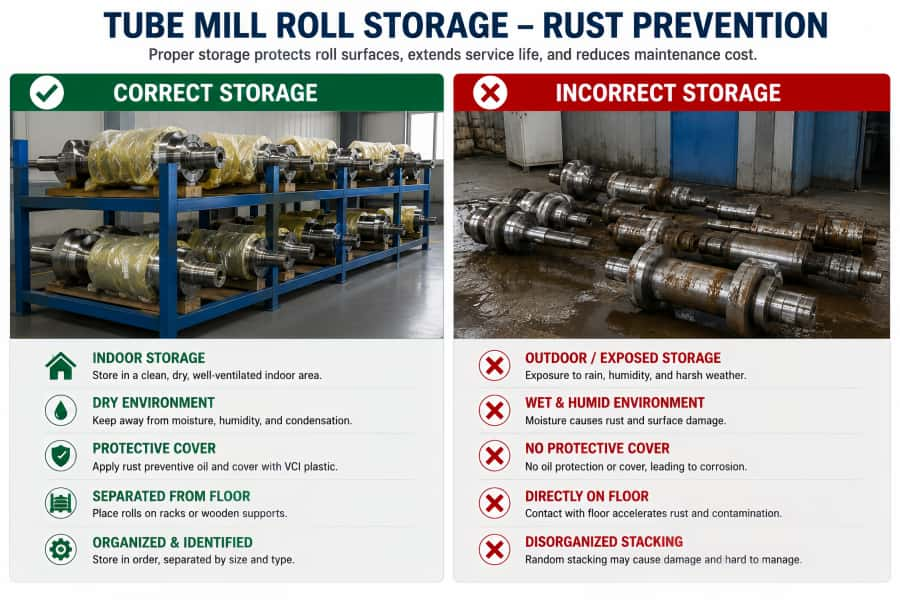
How Should Tube Mill Rolls Be Stored for Several Months?
The storage environment matters just as much as the anti-rust treatment.
A protected roll stored in a damp workshop can still develop corrosion. For long shutdowns, the rolls should preferably be kept indoors, away from direct water, condensation and corrosive materials. They should also be supported properly so that the working surface is not damaged during handling or storage.
Avoid putting precision rolls directly on a wet or damp concrete floor. If protective covers are used, they should not trap water against the roll surface.
This is especially worth checking after a major temperature change. A roll may look dry when it is covered, but condensation can develop underneath the covering if the surrounding environment becomes colder.
For a factory that shuts down regularly, it is useful to make roll storage part of the normal shutdown procedure rather than relying on individual operators to remember it each time.
How Often Should Stored Rolls Be Checked?
A roll that has been stored for a long time should not be forgotten.
For a short shutdown, there may be little need for repeated inspection. Once the storage period extends into weeks or months, however, checking the condition of the protective coating and storage environment becomes worthwhile.
Look for early signs rather than waiting for obvious rust:
- slight discoloration on the working surface
- damaged protective film
- moisture or condensation
- rust around grooves or edges
- deterioration of the anti-rust coating
- scratches caused by handling
- corrosion around exposed shaft areas
If corrosion is discovered early, the roll may only require cleaning and further protection. If the working surface has developed deeper pits or measurable damage, the situation is different and the roll should be assessed before being returned to production.
This is one reason why taking a few photographs before storage can be useful. It gives the maintenance team something to compare against when the tooling is inspected later.
What Should Be Checked Before the Tube Mill Starts Again?
The restart inspection deserves as much attention as the shutdown preparation.
Do not simply remove the cover, install the rollers and begin production.
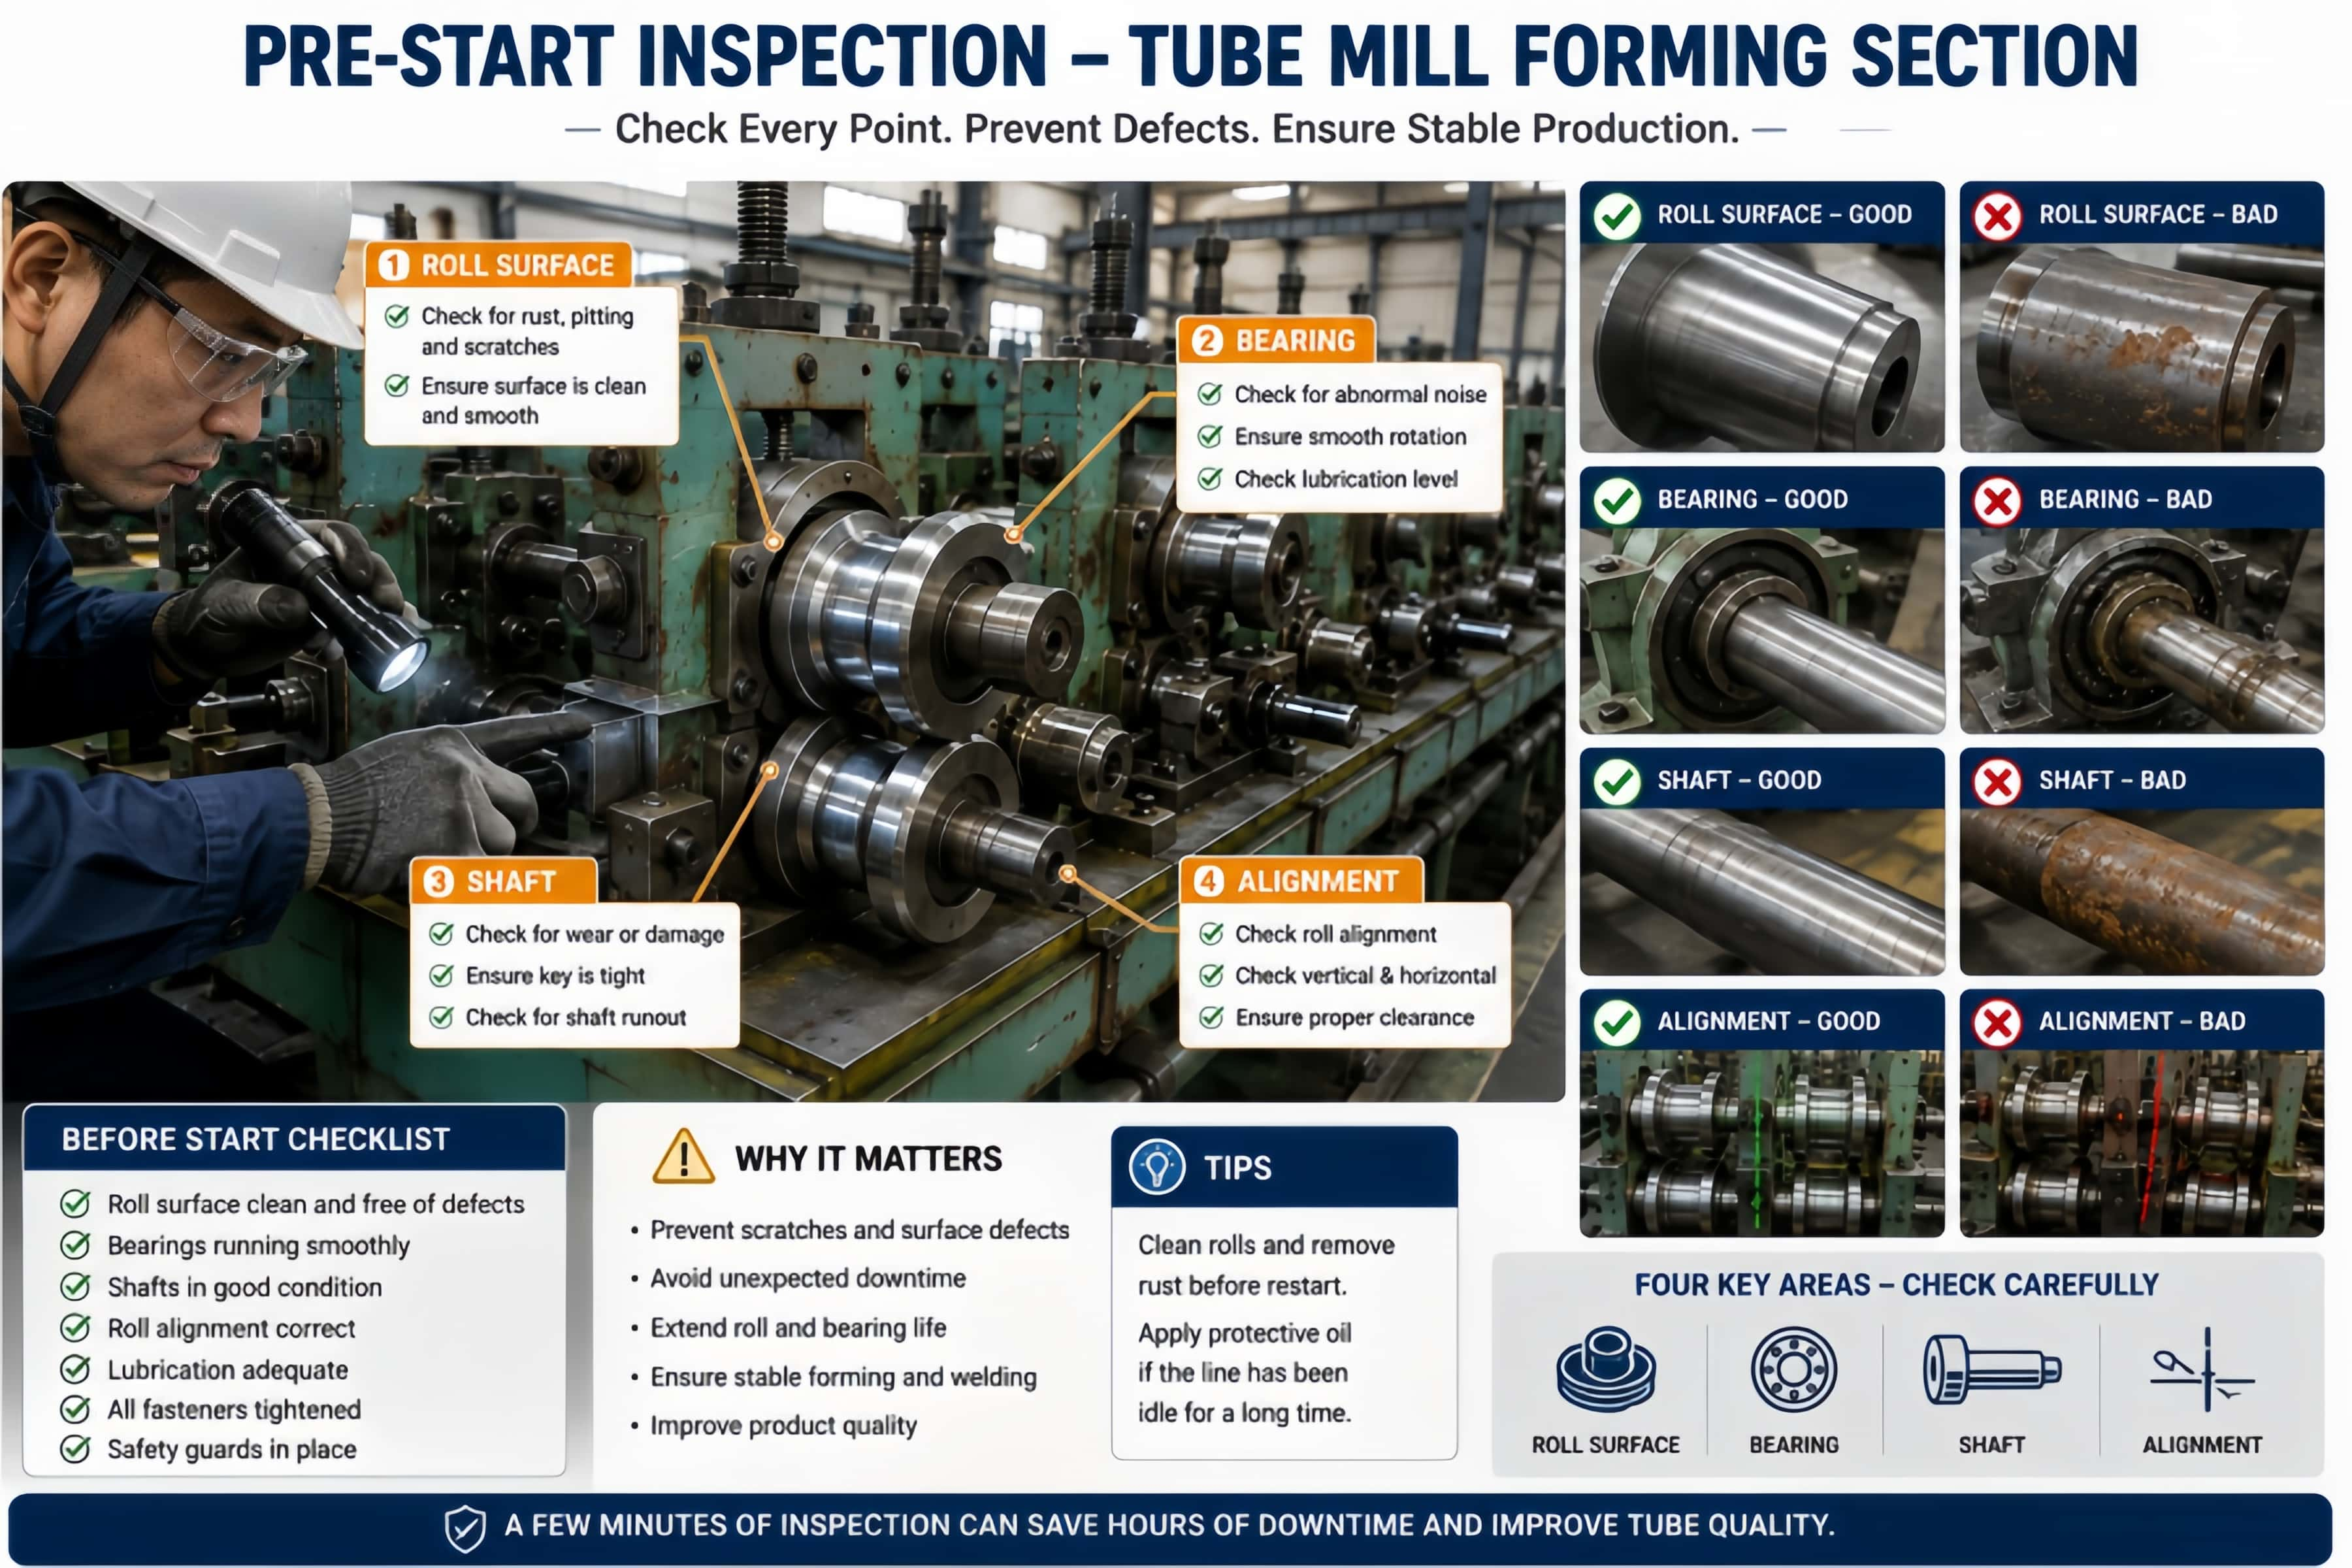
First check the working surface and remove any remaining storage coating according to the coating manufacturer's instructions. Look for rust, pitting, scratches and other changes that were not present before storage.
The roller itself is only part of the inspection. Check the shaft, bearings, mounting condition and alignment as well. If the rollers were removed from the machine during the shutdown, make sure they are installed at the correct position and that the forming setup has not changed.
This matters because a tube mill problem is not always caused by the welding section. Roller condition, bearing stability and alignment can influence how consistently the strip is formed before it reaches the welding area.
Changes in bearing condition can also affect shaft stability, roller alignment and eventually weld consistency. Our guide to tube mill bearing maintenance explains the common warning signs and inspection points in more detail.
After a long shutdown, it is better to run a controlled trial and inspect the first production tubes rather than assuming that everything is unchanged.
Should Anti-Rust Oil Be Applied to Tube Mill Rolls?
In most cases, yes, but the type and amount of protection should match the storage conditions.
A thin, even protective film can help prevent moisture from reaching an exposed steel surface. The important point is coverage. Pay attention to the roll grooves, edges, shaft areas and other exposed metal surfaces rather than only coating the easiest areas to reach.
There is also no reason to assume that more oil always means better protection. Excessive oil can collect dust and make the rolls unpleasant to handle later. The coating should be appropriate for the expected storage period and the manufacturer's recommendations should be followed.
For a short shutdown, such as a weekend or a few days, cleaning, drying and a suitable corrosion inhibitor may be enough. A machine that will remain idle for several months deserves more protection, particularly if the factory is humid.
For longer storage, VCI paper or film, sealed protective packaging and moisture-control measures can be considered in addition to the corrosion-preventive coating.
The objective is not to create a thick layer of oil. It is to keep moisture away from the metal surface for as long as the tooling remains out of service.
How Should Tube Mill Rolls Be Stored for Several Months?
The storage environment matters just as much as the anti-rust treatment.
A protected roll stored in a damp workshop can still develop corrosion. For long shutdowns, the rolls should preferably be kept indoors, away from direct water, condensation and corrosive materials. They should also be supported properly so that the working surface is not damaged during handling or storage.
Avoid putting precision rolls directly on a wet or damp concrete floor. If protective covers are used, they should not trap water against the roll surface.
This is especially worth checking after a major temperature change. A roll may look dry when it is covered, but condensation can develop underneath the covering if the surrounding environment becomes colder.
For a factory that shuts down regularly, it is useful to make roll storage part of the normal shutdown procedure rather than relying on individual operators to remember it each time.
Can Rust on a Roll Affect Tube Surface Quality?
It can, particularly when corrosion reaches the working profile.
A forming roll is not simply a rotating steel component. Its working surface has a specific geometry designed for a particular forming process. If corrosion removes material or creates pits, the surface condition is no longer the same as it was when the roll was manufactured.
Operators may then see roll marks, scratches or changes in forming behavior after the machine returns to production.
The severity depends on the depth and location of the corrosion. Light surface oxidation is very different from a damaged roll groove. A roll with significant pitting may need regrinding, and in some cases the remaining diameter or original profile may no longer allow the roll to be restored economically.
MIVI's tube mill maintenance guide notes that roll grinding can be used to recover accuracy, but the reduction in roll diameter needs to be considered because the rolling line height must be maintained after grinding.
So if a stored roll comes out of the warehouse with noticeable corrosion, it is better to inspect it before putting it back into the forming section.
When Should a Rusted Tube Mill Roll Be Reground or Replaced?
There is no useful rule that says every rusty roll must be replaced.
The decision depends on what happened to the working surface. A small amount of superficial oxidation may be removable. Deeper pitting, repeated surface marking or a significant change in the roll profile is a different matter.
The maintenance team should consider the original roll diameter, previous grinding history, surface hardness, actual corrosion depth and the dimensional requirements of the tube being produced.
For an older tube mill, replacement can also be an opportunity to review whether the original roll design still matches the current production requirements. Tube sizes, wall thicknesses, materials and production speeds may have changed over the years.
In that situation, simply copying an old roll without checking the current production conditions is not always the best approach.
Can MIVI Supply Replacement Tube Mill Rollers for an Existing Tube Mill?
Yes. This is particularly useful when an older tube mill is still mechanically sound but its forming rolls have reached the end of their useful service life.
In this situation, tube mill rollers can often be replaced without replacing the complete production line, provided that the existing machine configuration and roll requirements are properly evaluated.
MIVI provides customized tube mill solution for different tube sizes, materials, production requirements and existing machine configurations.
For replacement rollers, the engineering team can work from information such as:
- tube diameter or square/rectangular tube size
- wall thickness
- material grade
- existing roll drawing
- roll dimensions
- shaft dimensions
- machine model
- photographs of the existing tooling
- required production speed
If drawings are unavailable, photographs and measurements of the existing rolls can still provide useful starting information for an engineering review.
This is often more practical for an older production line than replacing the entire mill simply because the original tooling is worn or damaged.
A Simple Shutdown Routine for Tube Mill Roll Maintenance
For plants that want a practical routine, the process does not need to be complicated.
After the final production run, clean the forming rolls and remove coolant, steel particles and other residue. Dry the surfaces completely and inspect the grooves for abnormal wear or damage. Apply the appropriate corrosion protection, then move the rolls to a clean, dry storage location.
If the shutdown will last for several months, add protective packaging and moisture control where necessary. Check the rolls periodically rather than leaving them untouched until the day production resumes.
Before restarting the tube mill, inspect the rolls again, remove the storage protection, check the bearings and mounting condition, verify alignment, and inspect the first tubes produced after startup.
The routine may take some extra time at the beginning and end of a shutdown, but it is considerably easier than discovering a corroded roll after the line has already returned to production.
Final Thoughts
Tube mill roll maintenance during a shutdown is easy to underestimate because there is no immediate production problem to remind you about it.
In reality, the condition of the rolls while they are sitting idle can determine how smoothly the next production run starts.
A clean surface, proper corrosion protection and suitable storage conditions can prevent a relatively small maintenance issue from becoming a tooling problem later. For long shutdowns, periodic inspection is worth the effort, particularly in humid environments.
And when a roll has already suffered significant corrosion or wear, the question is no longer just how to protect it. The more useful question is whether the original roll can still meet the requirements of the current production line.
For manufacturers looking for replacement or customized tube mill rollers, MIVI can evaluate the existing tooling and production requirements and help determine a suitable roller solution.