


 Tube Mill Consumables: Inspection & Replacement Guide



How to Reduce Pipe Scrap Rate in Tube Mill Production? | ERW Guide
How to Reduce Scrap Rate in Tube Mill Production?
Quick Answer
The most effective way to reduce pipe scrap rate in tube mill production is to control three critical factors: weld quality, forming precision, and production speed stability.
Most tube mill scrap problems are not caused by one single component. They usually come from unstable strip feeding, incorrect roll adjustment, poor HF welding parameters, worn tooling, or inconsistent production speed. A reliable scrap reduction strategy requires optimizing the complete production process, including raw material preparation, forming section adjustm ent, welding control, sizing accuracy, and machine maintenance.
For ERW pipe manufacturers, reducing scrap rate means more than improving product quality. It directly reduces steel waste, production downtime, energy consumption, and labor cost. A well-designed tube mill with stable forming and welding performance can help factories achieve higher productivity and more consistent pipe quality.


What Causes High Scrap Rate in Tube Mill Production?
High scrap rate in a tube mill usually comes from problems occurring at different stages of production. Many factories only focus on the welding section after seeing weld cracks or leakage problems. However, the real cause may appear much earlier during strip preparation or forming.
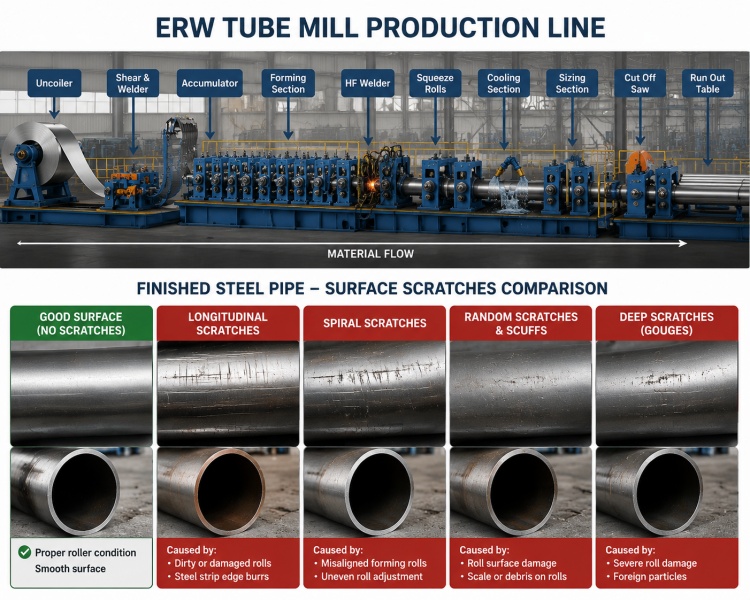
In ERW tube production, the steel strip passes through multiple processes:
Uncoiling → Strip Feeding → Forming → High Frequency Welding → Sizing → Cutting → Inspection
A defect created in an earlier stage often becomes more serious in later stages.
For example:
- Poor strip edge quality can create unstable welding conditions.
- Incorrect roll adjustment can cause tube deformation.
- Unstable line speed can change welding heat input.
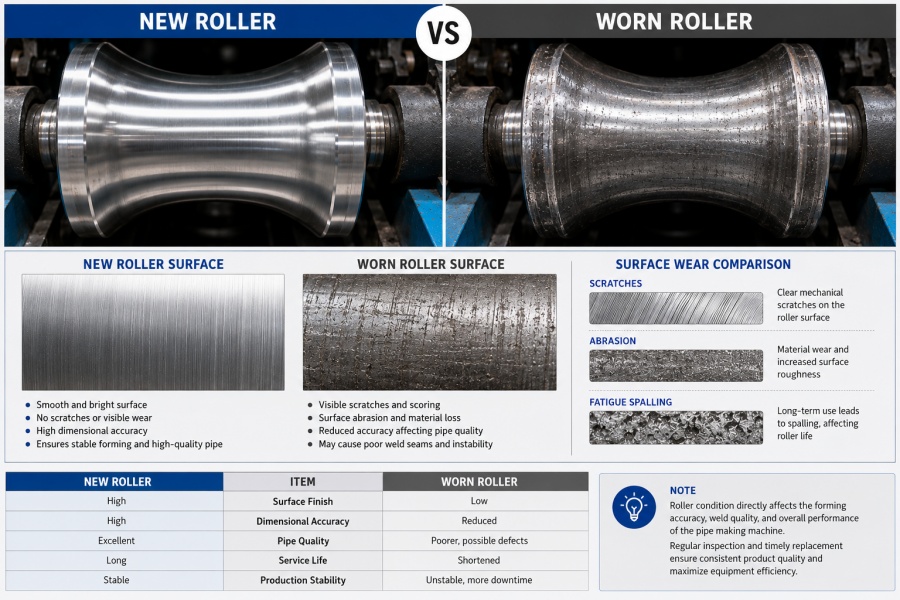
- Worn rollers can create surface scratches and dimensional problems.
Therefore, reducing pipe scrap rate requires a systematic approach instead of only adjusting welding parameters. Industry experience also shows that scrap reduction depends on tooling condition, raw material consistency, forming setup, welding parameters, and operator control.
Common Tube Mill Scrap Problems and Root Causes
| Scrap Problem | Possible Cause | Production Result |
|---|---|---|
| Weld seam opening | Incorrect HF power, unstable V angle, poor squeeze pressure | Pipe leakage, failed pressure test |
| Weld cracks | Excessive heat input, poor material quality | Reject pipes |
| Pipe dimension deviation | Incorrect roll adjustment | Customer rejection |
| Surface scratches | Roller damage or poor polishing | Appearance defects |
| Tube ovality | Poor sizing adjustment | Assembly problems |
| Cutting length error | Unstable flying saw control | Material waste |
How Can You Reduce Weld Defects in ERW Tube Production?
Reducing weld defects is one of the fastest ways to reduce pipe scrap rate because welding problems usually create complete pipe rejection.
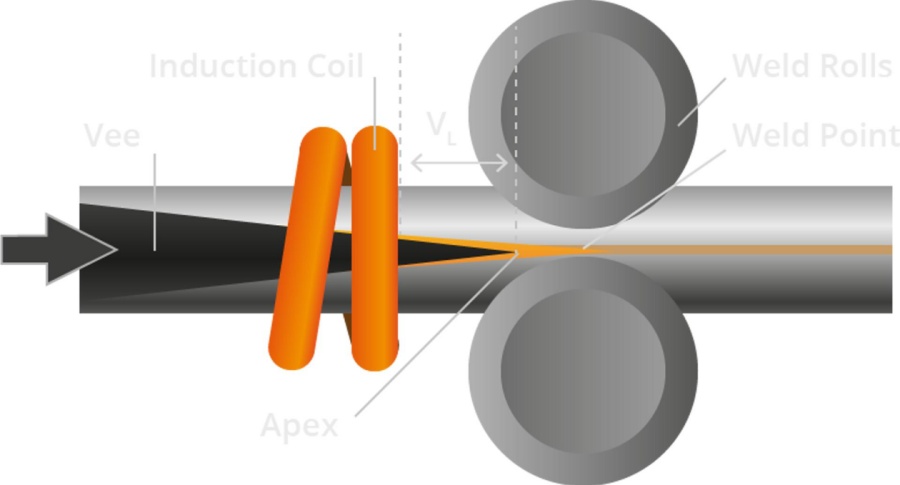
In HF welded tube mills, welding quality depends on the relationship between:
- Welding power
- Welding speed
- Material grade
- Wall thickness
- V-angle condition
- Impeder position
- Squeeze roller pressure
Many factories make the same mistake:
They increase welding power when weld quality becomes unstable.
However, the welding section is only the final step. If the strip edges are not correctly prepared before welding, increasing power cannot fully solve the problem.
How Does HF Welding Parameter Adjustment Affect Scrap Rate?
High frequency welding requires balanced energy input.
When welding power is too low:
The common results include:
- insufficient fusion
- weak weld seam
- leakage during hydro testing
- pipe bursting during flattening test
When welding power is too high:
The problems may include:
- excessive heating
- large internal bead
- material overheating
- weld cracking
The correct welding condition should match:
- tube diameter
- wall thickness
- steel grade
- production speed
For example:
A thin-wall carbon steel tube running at high speed requires completely different welding parameters compared with a thick-wall structural pipe.
Therefore, operators should not use the same welding setting for different tube sizes.
Why Does Forming Precision Affect Tube Mill Scrap Rate?
Many manufacturers believe welding is the main reason for pipe defects.
However, from actual production experience, many welding problems are created before the tube reaches the welding station.
The forming section determines whether the strip edges can meet correctly before HF welding.
If forming accuracy is poor, problems appear:
- unstable seam alignment
- changing V-angle
- uneven edge contact
- inconsistent welding condition
This means:
Better forming precision creates better welding stability.
A tube mill cannot achieve stable welding performance if the forming section continuously changes the tube geometry.
What Problems Are Caused by Poor Tube Mill Forming?
1. Incorrect Roll Pass Design
Every tube size requires suitable roll tooling design.
If the forming process is too aggressive:
- strip deformation increases
- edge stress increases
- welding becomes unstable
If forming is too weak:
- tube shape cannot be controlled
- sizing section must correct excessive deformation
2. Roller Alignment Problems
Even high-quality rollers cannot perform correctly if alignment is inaccurate.
Common problems:
- upper and lower rollers are not centered
- roller gap is incorrect
- shaft movement exists
- bearing wear affects stability
The result:
- pipe diameter fluctuation
- surface scratches
- increased adjustment time
From factory experience, some customers initially tried to solve weld defects by replacing HF welding components. After inspection, the actual problem was roller alignment and forming instability.
This is a common situation:
The welding problem was only a symptom. The forming section was the real cause.

How Can Tube Mill Rollers Help Reduce Pipe Scrap Rate?
Tube mill rollers directly influence:
- forming accuracy
- pipe surface quality
- production stability
- size changeover efficiency
A good roller design should consider:
- tube diameter range
- wall thickness
- material strength
- forming pass sequence
- production speed
Poor tooling can create hidden costs:
- more trial production
- more adjustment time
- higher material waste
- shorter roller life
For manufacturers producing different products such as:
- carbon steel pipes
- galvanized pipes
- stainless steel tubes
- square and rectangular tubes
customized roll design becomes especially important.
How Can Speed Stability Reduce Tube Mill Scrap?
Production speed is one of the most important variables affecting scrap rate in an ERW tube mill.
Many manufacturers naturally focus on increasing line speed because higher speed means more theoretical output. However, maximum speed and maximum qualified production are not the same thing.
A tube mill running at 120 m/min with frequent weld defects, dimensional variation, and stoppages may produce less qualified pipe per shift than a line running at a slightly lower but stable speed.
The real objective is therefore:
Do not simply maximize tube mill speed. Stabilize the speed at which the line can continuously produce qualified pipe.
In HF-ERW production, line speed is closely related to welding heat input, forming stability, squeeze conditions, and downstream sizing. MIVI's technical analysis also emphasizes that line speed, HF welding power, V-angle, squeeze pressure, and heating length must be considered together rather than treated as isolated settings.
How Does Tube Mill Speed Affect Welding Stability?
When production speed changes, the amount of energy delivered to a given length of strip also changes.
For a simplified production analysis:
Higher line speed + unchanged welding power → lower heat input per unit length
Lower line speed + unchanged welding power → higher heat input per unit length
This does not mean that there is one universal relationship or one fixed power setting for every tube. The actual working window depends on material, wall thickness, tube diameter, V-angle, welding frequency, squeeze condition, and other machine variables.
The important point is that the welding system must remain inside a stable process window.
When operators increase speed without adjusting the overall process, several problems can appear:
- incomplete fusion
- unstable weld seam
- insufficient heating
- inconsistent weld bead
- increased flattening-test failures
- higher rejection rate
On the other hand, slowing the line excessively to “fix” the weld may increase heat input too much and create overheating or other defects.
This is why speed should be optimized together with welding conditions, rather than treated as an independent production target.
Why Can Frequent Speed Fluctuation Increase Pipe Scrap?
A stable tube mill is easier to control than a tube mill that continuously accelerates and decelerates.
Imagine a production line where the target speed is 80 m/min, but actual speed repeatedly moves between 65, 80, and 95 m/min.
Even when the average speed appears normal, the process is not stable.
Every speed change can influence:
- heat input
- welding condition
- strip tension
- forming behavior
- cooling time
- sizing condition
- cutting synchronization
The operator may then compensate manually.
For example:
Speed decreases
↓
Welding becomes hotter
↓
Operator reduces power
↓
Speed increases again
↓
Heating becomes insufficient
↓
Operator increases power
↓
Cycle repeats
This creates a production environment in which operators are constantly chasing the process instead of controlling it.
The better approach is to identify why the speed changes occur.
Possible causes include:
- unstable drive control
- strip feeding variation
- uncoiler problems
- accumulator instability
- mechanical resistance
- bearing problems
- poor synchronization
- control-system issues
How Should You Stabilize Tube Mill Speed?
Before increasing maximum line speed, check the complete material path.
1. Check strip feeding stability
The strip should enter the forming section smoothly and consistently.
Uneven feeding can create tension variation, which affects forming and welding.
2. Check the accumulator or storage system
The accumulator should provide stable strip supply during coil preparation and transition.
An unstable storage system can transfer material fluctuation into the forming section.
3. Check drive and transmission systems
Inspect:
- motors
- gearboxes
- couplings
- encoders
- bearings
- speed feedback
If speed feedback is inaccurate, automatic control becomes less effective.
4. Check mechanical resistance
A worn bearing or damaged component can create additional resistance.
At low speed the problem may be difficult to notice.
At high speed it can become much more obvious.
5. Check synchronization
The forming section, welding system, sizing section, and flying saw should operate as one coordinated production system.
How Do Raw Materials Influence Scrap Rate?
Raw material quality is one of the most underestimated causes of tube mill scrap.
When a tube manufacturer sees weld defects, the first reaction is often to inspect:
- HF power
- induction coil
- ferrite rod
- impeder
- squeeze rollers
These are important.
But the strip entering the machine may already have characteristics that make stable production difficult.
MIVI's recent project analysis specifically points out that variations in strip edge quality, thickness consistency, and surface condition can affect forming and welding stability before the material reaches the welding zone.
This leads to an important troubleshooting rule:
Do not assume every tube defect is caused by the tube mill.
How Does Strip Thickness Variation Increase Scrap?
A tube mill is normally configured around a specified material thickness.
When strip thickness changes significantly within a coil or between coils, forming and welding conditions can change.
Possible results include:
- changing forming force
- different edge behavior
- inconsistent welding conditions
- dimensional variation
- increased adjustment requirements
For factories producing multiple wall thicknesses, incoming material inspection becomes even more important.
Record at least:
- nominal thickness
- measured thickness
- strip width
- coil number
- material grade
This information becomes extremely useful when a quality problem appears later.
Why Does Strip Edge Quality Matter for ERW Welding?
The two strip edges eventually become the longitudinal weld.
Therefore, the condition of these edges directly affects the welding process.
Common problems include:
- excessive burr
- uneven trimming
- edge cracking
- rust
- oil contamination
- mechanical damage
- inconsistent edge geometry
When the strip edges are not properly prepared, the welding process may become less stable.
The operator may then increase welding power or squeeze force to compensate.
That can hide the original problem temporarily without removing its root cause.
MIVI's technical content also identifies burrs, rust, uneven trimming, and strip-width fluctuation as raw-material conditions that can contribute to unstable ERW welding and forming.
Can Steel Chemistry Affect Tube Mill Scrap?
Yes.
Material chemistry can influence forming and welding behavior.
For example, changes in carbon content and other elements can alter material properties and welding response. Therefore, two coils sold under the same nominal material grade may still behave differently enough to require process attention.
When a scrap problem suddenly begins after changing coils, engineers should not immediately assume that the machine changed.
Ask:
What changed before the defect appeared?
Possible answers include:
- coil supplier
- material grade
- strip thickness
- strip width
- edge preparation
- surface condition
- coil batch
This simple question can prevent unnecessary machine adjustments.
How Can You Identify Whether Scrap Comes From Raw Material or the Machine?
The easiest approach is to correlate defects with production events.
| Production Observation | Likely Direction | First Things to Check |
|---|---|---|
| Problem occurs only with one coil | Raw material | Thickness, width, edge, chemistry |
| Problem occurs with every coil | Machine/process | Forming, welding, alignment |
| Problem begins after speed increase | Process parameter | Speed, power, squeeze |
| Problem appears after tube-size change | Tooling/setup | Roll pass, roll gap, alignment |
| Problem develops gradually | Mechanical wear | Rollers, bearings, guides |
| Problem appears intermittently | Control/mechanical | Drives, feedback, alignment |
This diagnostic method is more useful than simply recording “welding problem.”
A professional production report should record:
When → Where → With Which Coil → At What Speed → Under Which Settings
That information gives engineers a much clearer starting point.
What Does a Real Tube Mill Scrap Problem Look Like?
Factory Experience Case Study: The Weld Problem That Was Not Caused by HF Power
Consider a typical production situation.
A factory was producing carbon steel tubes and noticed that some pipes began failing the flattening test.
The external weld appearance was generally acceptable.
The first response was to adjust welding power.
After increasing power, the defect rate temporarily decreased.
The operator then reduced production speed.
Again, the weld appeared more stable.
But the factory had now lost production efficiency.
The problem later returned.
Instead of continuing to adjust power and speed, the maintenance team inspected the complete forming and welding section.
The investigation focused on:
- squeeze roller condition
- roller alignment
- bearing clearance
- strip edge condition
- V-angle stability
- production speed
The inspection showed that the squeeze section was not maintaining consistent mechanical conditions.
This matters because ERW welding is not controlled by electrical power alone.
The welding process is a combination of:
Heat Input + Edge Preparation + Forming + Squeeze + Speed
MIVI's own technical case analysis describes how worn squeeze rolls, alignment changes, bearing clearance, raw-material inconsistency, and changes in line speed can contribute to weld instability even when the operator has not changed the main welding setting.
The lesson is important:
When a weld defect appears, check the complete process before changing one parameter repeatedly.
Why Did Changing Welding Power Only Temporarily Solve the Problem?
Increasing welding power can help when the actual problem is insufficient heat input.
But suppose the real problem is:
Poor forming → unstable V-angle → inconsistent edge contact
Increasing HF power cannot permanently correct the forming problem.
Likewise:
Worn squeeze roller → unstable forging pressure → inconsistent weld
Increasing power may only compensate temporarily.
This explains why some factories repeatedly experience the same weld problem even after:
- replacing ferrite rods
- increasing welding power
- slowing production speed
- replacing induction coils
The problem may have originated mechanically upstream.
What Should Engineers Record During Scrap Troubleshooting?
A simple production log can greatly improve diagnosis.
Record:
| Parameter | Record |
| Tube OD | Actual size |
| Wall thickness | Actual/nominal |
| Material | Grade |
| Coil number | Identification |
| Line speed | Actual |
| HF power | Actual |
| V-angle | Production condition |
| Squeeze setting | Actual |
| Weld appearance | Observation |
| Defect location | Before/after welding |
| Scrap type | Weld/forming/cutting |
| Operator adjustment | What changed |
After several production runs, patterns often become visible.
For example:
Scrap only appears after the speed exceeds a certain production condition.
That points toward a process window.
Or:
Scrap only appears with one supplier's coils.
That points toward raw material.
Or:
Scrap gradually increases as the tooling continues to run.
That points toward wear.
This is much stronger than making adjustments based on intuition alone.
How Can MIVI Equipment Solutions Help Reduce Tube Mill Scrap?
MIVI's solution should be positioned around process stability, rather than simply machine specifications.
The objective is not:
“Buy a more powerful machine.”
The objective is:
Build a tube production system that consistently produces qualified pipes with predictable forming, welding, sizing, and cutting performance.
This is where the product section should account for roughly 20% of the article, while the other 80% remains focused on diagnosis and technical education.
How Can Precision Forming Help Reduce Scrap?
The forming section establishes the tube geometry before welding.
If the geometry is unstable, welding becomes more difficult.
A precision forming system should focus on:
- roll pass design
- roller alignment
- roll gap
- guide adjustment
- shaft condition
- bearing condition
- material compatibility
For different products, tooling requirements can be different.
Round carbon-steel tubes, stainless-steel tubes, square tubes, and rectangular tubes do not necessarily use the same forming strategy.
MIVI can provide customized roll design based on the required tube dimensions, material, wall thickness, and forming requirements.
【Internal Link: Custom Tube Mill Rollers for Square and Rectangular Pipes → Link to MIVI Tube Mill Roller Customization page】
How Can MIVI Tube Mill Rollers Support Forming Accuracy?
Rollers are not simply wear parts.
They are part of the forming system.
A properly designed roll pass should gradually transform the strip into the required tube geometry instead of forcing excessive deformation in one stage.
MIVI can highlight its engineering capabilities in:
- CAD drawing
- roll-pass design
- customized tooling
- machining
- surface finishing
- application-based roller selection
The key benefit to the end user is not just “high-quality rollers.”
The benefit is:
More predictable forming → more stable edge alignment → more consistent welding → lower rejection risk.
【Internal Link: Tube Mill Rollers → Link to MIVI Tube Mill Roller product page】
How Can Stable HF Welding Reduce Pipe Scrap?
The HF welding section should be considered together with forming and squeeze.
A typical HF welding system includes:
- induction coil
- HF power system
- ferrite rod
- impeder
- squeeze rollers
- welding controls
- cooling system
Each component has a role.
For example, the impeder helps concentrate electromagnetic energy around the weld area, while squeeze rollers mechanically forge the heated edges together.
A weak weld may therefore be related to:
- insufficient heat
- excessive heat
- poor edge condition
- incorrect V-angle
- insufficient squeeze
- excessive squeeze
- speed instability
- mechanical wear
Why Is Speed Stability Important in MIVI Tube Mill Design?
For production-line buyers, the important question is not only:
“What is the maximum line speed?”
A better procurement question is:
How stable is the line under continuous production?
MIVI's equipment solution can therefore be presented around:
- stable strip feeding
- forming precision
- welding stability
- synchronized speed control
- reliable sizing
- cutting synchronization
- maintainability
The value for the customer is not just higher nominal speed.
It is:
Higher qualified output with less unnecessary scrap and downtime.
How Should You Measure the Result After Reducing Scrap?
A scrap-reduction project needs measurable KPIs.
The basic calculation is:
Scrap Rate = Rejected Pipe Weight ÷ Total Production Weight × 100%
However, one number is not enough.
Track:
| KPI | Why It Matters |
| Weld rejection rate | Measures welding stability |
| Dimensional rejection | Measures forming/sizing quality |
| Surface rejection | Indicates tooling condition |
| Cutting waste | Measures saw synchronization |
| Rework rate | Indicates process instability |
| Downtime | Measures equipment reliability |
| Speed variation | Measures production stability |
| Qualified output | Measures actual production performance |
The most useful business metric is often not “maximum speed.”
It is:
Qualified tons produced per shift.
A slightly slower line with substantially lower rejection can create more usable output than a faster line with unstable quality.
What Is the Best Step-by-Step Method to Reduce Pipe Scrap Rate?
A practical approach is to follow this sequence.
Step 1: Identify the largest scrap category
Start with actual production records.
Do not guess.
Determine whether most rejected pipes are caused by:
- weld defects
- dimension problems
- scratches
- cutting errors
- material issues
Step 2: Find the location where the problem begins
Ask:
Where does the defect first appear?
Is it:
- before forming?
- during forming?
- at the welding point?
- after sizing?
- during cutting?
- during testing?
Step 3: Check what changed
Check:
- coil
- tube size
- speed
- welding power
- tooling
- operator
- maintenance condition
Step 4: Inspect upstream causes
Do not assume the final defect location is the root cause.
A weld defect may originate in forming.
A dimension problem may originate in tooling.
A speed problem may originate in the drive system.
Step 5: Change one major parameter at a time
If operators change speed, HF power, squeeze pressure, and roller adjustment simultaneously, it becomes difficult to identify the actual cause.
Controlled adjustment produces better engineering information.
Step 6: Verify the result using production data
Compare:
Before vs After
not simply:
Looks better vs Looks worse
FAQ
What is the fastest way to reduce pipe scrap rate?
The fastest approach is to identify the largest source of rejection first and determine where the defect begins. For ERW tube mills, common causes include welding instability, poor forming precision, roller misalignment, speed fluctuation, and inconsistent raw material.
Why does my tube mill have a high scrap rate?
A high scrap rate can result from problems in welding, forming, sizing, cutting, raw material, tooling, or machine control. The correct solution should be based on the defect type and production conditions rather than changing welding power alone.
Can reducing tube mill speed reduce scrap?
Reducing speed can sometimes improve weld stability when heat input is insufficient, but it is not a universal solution. The correct approach is to optimize speed together with HF power, forming conditions, V-angle, and squeeze force.
Can tube mill rollers affect welding quality?
Yes. Rollers determine how the strip is formed and how the edges approach the welding point. Poor roll design, misalignment, wear, or incorrect adjustment can create unstable edge contact and contribute to weld problems.
How does raw material affect ERW pipe quality?
Strip thickness, width, edge condition, surface condition, and material properties can affect forming and welding stability. When defects appear only with specific coils or material batches, incoming material should be investigated.
Does increasing HF welding power reduce scrap?
Not necessarily. Increasing HF power can help when heat input is insufficient, but excessive heating can also create defects. HF power should be evaluated together with line speed, V-angle, squeeze force, strip condition, and forming stability.
How do you calculate tube mill scrap rate?
A basic formula is:
Scrap Rate = Rejected Pipe Weight ÷ Total Production Weight × 100%
Manufacturers should also track weld rejection, dimensional rejection, surface defects, cutting waste, rework, and downtime.
Can replacing tube mill rollers reduce scrap?
Replacing worn or incorrectly designed rollers can reduce scrap when forming instability, surface damage, or dimensional problems are caused by the tooling. However, roller replacement will not solve every type of scrap problem.
Can a new ERW tube mill reduce production scrap?
A new ERW tube mill can improve scrap performance when the existing machine has limitations in forming precision, welding control, speed stability, automation, or mechanical condition. However, raw material problems and incorrect operating parameters must also be addressed.