


 Tube Mill Consumables: Inspection & Replacement Guide




Power vs Squeeze Force in ERW Welding: Finding the Right Balance for Stable Tube Production
Introduction
If you’ve spent enough time around an ERW tube mill, you know welding problems rarely appear without warning.
Usually, the first signs are small.
A few unusual sparks near the V-point.
A slightly heavier burr.
Maybe the weld seam color looks different from normal.
At first, production continues.
Then problems start showing up.
Hydro testing begins to fail.
Flattening cracks appear.
Sometimes the weld opens unexpectedly.
When this happens, many operators immediately look at the HF welder.
They check power settings.
They adjust frequency.
Some even increase power, hoping more heat will solve the issue.
Sometimes that helps.
Very often, it doesn’t.
In fact, after working with many tube manufacturers, one pattern shows up repeatedly: the real problem is not always welding power.
Quite often, it comes from unstable squeeze force.
That’s why understanding the relationship between welding power and ERW squeeze force matters so much.
Too little squeeze force creates weak bonding.
Too much squeeze force creates excessive upset, roller wear, and unstable weld seams.
The best weld quality comes from balance—not simply higher power or higher pressure.
This is especially true in high-speed carbon steel pipe production, where small parameter changes can quickly affect weld stability.
At MIVI Tube Machine, our engineers often see customers focus heavily on electrical parameters while overlooking mechanical instability in the squeeze section.
That's usually where the hidden problem begins.
Quick Answer Table
| Condition | Common Problem | Production Result |
|---|---|---|
| Power too high | Overheating | Burned weld |
| Squeeze force too low | Weak forging | Cold weld |
| Squeeze force too high | Excessive upset | Large burr |
| Balanced parameters | Stable welding | Strong weld |
Why More Welding Power Doesn’t Always Solve Welding Problems
One of the most common mistakes in ERW production is assuming that weak welding always means insufficient power.
It sounds logical.
If the weld isn't strong enough, add more power.
But production doesn't always work that way.
We've seen many cases where increasing power actually made welding less stable.
A customer once reported weak weld strength on a carbon steel tube line. Their first reaction was to raise HF output.
Initially, sparks became more visible.
The weld zone looked hotter.
Everything seemed better.
A few hours later, burr became larger. Weld discoloration increased. Hydro test failure became more frequent.
The problem wasn’t lack of heat.
It was too much heat.
More specifically, too much heat entering the V area before the strip edges reached proper squeeze.
That changes everything.
Instead of controlled forge welding, the strip edges become overheated. Excessive oxidation occurs, and molten metal starts ejecting before the squeeze rolls can properly forge the edges together.
This usually creates unstable welding behavior.
Common symptoms include:
- Large irregular sparks
- Burned weld seam
- Excessive outside burr
- Heavy oxidation
- Rough weld bead
When these symptoms appear, increasing power further usually makes the situation worse.
Common Problems Caused by Excessive Welding Power
| Symptom | Likely Cause | Result |
|---|---|---|
| Large sparks | Overheating | Unstable welding |
| Burned seam | Excess power | Weak weld |
| Oxidation | Excessive heat | Poor bonding |
| Heavy burr | Poor heat balance | Material waste |
Another issue is that excessive power often hides the real problem.
For example:
- Poor V-angle
- Worn squeeze rolls
- Improper coil position
- Weak impeder performance
Operators may think they solved the issue by increasing power.
In reality, they only masked the root cause.
Sooner or later, defects return.
This is why a stable welding process depends on more than electrical power alone.
Mechanical stability matters just as much.
A reliableHigh Frequency Welding Machinehelps maintain consistent heat input, but even the best welding system cannot compensate for poor squeeze control.
That balance is what determines weld quality.
Field Experience from MIVI Engineers
In many older production lines, especially mills with worn roll assemblies, weld instability often starts in the squeeze section rather than in the welder itself.
This is something our engineers regularly observe during machine diagnosis.
A tube mill may still run.
Production speed may remain acceptable.
But once squeeze roll alignment becomes inconsistent, welding stability becomes difficult to control.
The operator adjusts power repeatedly.
The real issue remains unresolved.
That's why power adjustment should never be the only solution.
The squeeze section must be evaluated together.
Low Squeeze Force: A Common Cause of Weak Welds
Compared with excessive power, low squeeze force is often harder to identify.
Why?
Because the weld can look normal on the outside.
That’s what makes this problem dangerous.
The weld bead may appear acceptable.
Sparks may not look abnormal.
Line speed may stay stable.
Everything seems fine.
Until testing begins.
Then defects appear.
Hydro leakage.
Flattening cracks.
UT indications.
This happens because the strip edges were heated, but not forged together with enough pressure.
That means bonding remained incomplete.
Inside the weld seam, oxides can become trapped between the strip edges.
Externally, everything looks acceptable.
Internally, the weld is weak.
This type of defect is common in:
- Thin wall production
- High-speed lines
- Worn squeeze sections
- Poor roll alignment
The root issue is simple.
Heat alone does not create a strong ERW weld.
Pressure completes the weld.
Without enough squeeze force, proper forge bonding cannot happen.
Common Problems Caused by Low Squeeze Force
| Problem | Root Cause | Production Risk |
|---|---|---|
| Cold weld | Low pressure | Weak seam |
| Poor bonding | Insufficient squeeze | Hydro failure |
| Oxide inclusion | Weak forging | Internal defect |
| Seam cracking | Incomplete weld | Customer complaint |
his is why ERW squeeze force is so critical.
It determines whether heated strip edges actually bond into a strong weld seam.
At this stage, even a small pressure variation can create major differences in weld quality.
That's especially true in high-speed production.
A stable ERW Tube Mill Machineplays a major role here.
Machine rigidity, shaft stability, bearing condition, and squeeze roll precision all affect pressure consistency.
If the squeeze section vibrates or alignment drifts, pressure becomes unstable.
Then weld quality becomes unpredictable.
A Problem Many Operators Overlook
Here’s something we see often.
An operator notices weak welds.
He increases power.
The weld still fails.
Then he increases squeeze pressure aggressively.
Now burr becomes excessive.
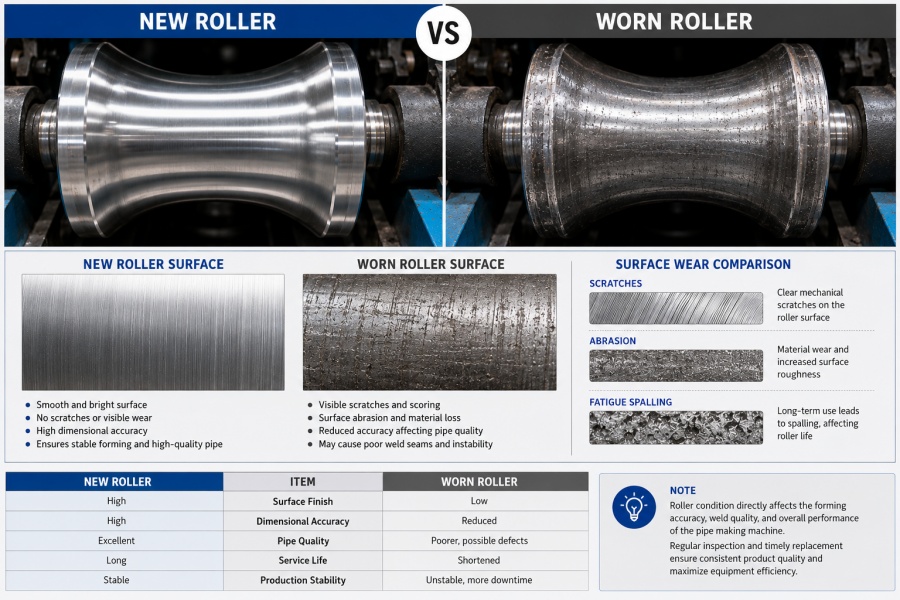
Roller wear accelerates.
The line becomes even less stable.
At that point, both power and pressure are out of balance.
This is where many welding problems become difficult to diagnose.
Because once multiple parameters drift together, the original root cause becomes harder to identify.
That’s why experienced engineers usually evaluate these factors together:
- Welding power
- Squeeze force
- V-angle
- Line speed
- Roll condition
Looking at only one parameter rarely solves the problem.
The welding system works as a complete process.
Not as isolated settings.
Too Much Pressure Can Also Create Problems
In tube production, there is another common misunderstanding.
Some operators believe:
If low squeeze force causes weak welds, then increasing pressure should always improve weld quality.
That sounds reasonable.
But in actual production, too much pressure creates a different set of problems.
And sometimes, those problems are even harder to deal with.
Over-squeeze is especially common in factories where operators try to compensate for unstable welding by mechanically increasing roll pressure.
At first, the weld may appear stronger.
But after some time, new issues begin to show.
The burr becomes larger.
The weld bead gets rough.
Roller wear accelerates.
Eventually, production stability starts dropping.
What Happens During Over Squeeze?
When squeeze force becomes too high, excessive metal is forced outward during forging.
This creates too much upset.
The result is not better welding.
Instead, the weld zone becomes mechanically unstable.
Typical symptoms include:
- Excessive outside burr
- Large weld upset
- Poor bead shape
- Surface deformation
- Increased roll wear
Common Problems Caused by Over Squeeze
| Problem | Cause | Result |
|---|---|---|
| Large burr | Excessive squeeze | Material waste |
| Rough weld bead | Over forging | Surface defects |
| Roller wear | High mechanical load | Maintenance cost |
| Bearing stress | Excess pressure | Shorter machine life |
This problem becomes more serious in high-speed production lines.
Why?
Because at high line speed, even small pressure changes can cause large differences in metal flow.
That means excessive squeeze force can quickly destabilize the weld seam.

MIVI Field Experience
At MIVI, we've seen this issue often on older tube mills.
Especially when:
- squeeze rolls are worn
- bearings have clearance
- shafts have vibration
Operators increase pressure to compensate.
That creates a chain reaction.
First, burr increases.
Then roller wear becomes faster.
Soon, weld consistency starts dropping.
The real issue is no longer just welding.
It becomes a mechanical stability problem.
That's why stable squeeze force depends heavily on machine rigidity and roll precision.
A reliableTube Mill Mould and properly aligned squeeze rolls make a major difference.
H2 How to Find the Right Welding Balance
This is the question every tube manufacturer wants to answer.
What is the best balance between welding power and ERW squeeze force?
Unfortunately, there is no universal number.
The ideal setting depends on multiple production factors.
Such as:
- Tube diameter
- Wall thickness
- Steel grade
- Production speed
- V-angle
- Welding frequency
That’s why experienced operators rarely rely on a fixed parameter.
Instead, they focus on welding balance.
What Does Good Welding Balance Look Like?
When power and squeeze force are properly balanced, welding becomes stable.
You usually see:
- Smooth sparks
- Stable weld seam
- Consistent burr size
- Strong weld bonding
- Low defect rate
The production line runs smoothly.
Testing results remain stable.
Customer complaints drop.
Best Welding Balance Table
| Parameter | Too Low | Too High | Ideal Condition |
|---|---|---|---|
| Welding Power | Weak heating | Overheating | Stable heat |
| Squeeze Force | Weak forging | Excess upset | Proper bonding |
| Line Speed | Low output | Unstable welding | Balanced production |
The goal is simple.
Heat the strip edges to proper forging temperature.
Then apply enough squeeze force to remove oxides and achieve complete bonding.
No more.
No less.
That balance creates stable welding.
Key Factors That Affect Welding Balance
| Factor | Influence |
|---|---|
| Tube size | Affects squeeze force |
| Wall thickness | Affects heating |
| Material grade | Affects welding behavior |
| Production speed | Affects heat input |
A stable Round Pipe Production Line usually maintains better welding consistency because machine alignment and process stability are stronger.
This is especially important for manufacturers producing structural pipes at high speed.

How to Check If Weld Quality Is Really Good
This is another important point.
Good weld appearance does not always mean good weld quality.
This is where many factories make mistakes.
The weld seam looks fine.
Production continues.
Then customer complaints appear later.
That’s why inspection matters.
Reliable testing confirms whether welding quality is truly stable.
There are three main inspection methods used in ERW tube production.
Hydro Test
Hydro testing checks whether the pipe can withstand internal pressure.
It helps identify:
- Leakage
- Seam cracks
- Weak bonding
If squeeze force is too low, hydro test failure becomes common.
This is usually the first sign of weak weld bonding.

Flattening Test
Flattening test evaluates weld ductility.
The pipe is compressed until deformation occurs.
This test helps reveal:
- Weld cracking
- Seam opening
- Brittle fracture
A weak weld usually fails quickly during flattening.

UT Inspection
Ultrasonic testing is essential for detecting internal defects.
This includes:
- Lack of fusion
- Oxide inclusion
- Internal cracks
This method is especially important for high-quality structural and industrial pipes.
Because some weld defects cannot be seen from the surface.
Inspection Summary Table
| Test Method | Detects | Main Purpose |
|---|---|---|
| Hydro Test | Leakage | Pressure resistance |
| Flattening Test | Cracks | Weld ductility |
| UT Inspection | Internal defects | Weld integrity |
At this stage, testing results tell the real story.
Not appearance.
Not sparks.
Not assumptions.
Good weld quality must be verified through reliable inspection.
How MIVI Tube Mills Improve Welding Stability
After analyzing welding power and ERW squeeze force, one thing becomes clear.
Stable welding is not only about parameter adjustment.
Machine stability matters just as much.
Even experienced operators struggle to maintain consistent weld quality when the machine itself lacks rigidity, alignment precision, or stable squeeze pressure.
This is why equipment quality plays such a critical role in ERW production.
A tube mill with poor structural stability often creates recurring welding problems.
At first, those problems may appear small.
A little vibration.
Slight roll misalignment.
Minor bearing clearance.
But under continuous production, these small mechanical issues become much bigger.
They affect:
- Squeeze pressure consistency
- Weld seam stability
- Burr control
- Product quality
Eventually, they increase:
- Scrap rate
- Downtime
- Maintenance cost
What Makes a Tube Mill Suitable for Stable ERW Welding?
A reliable ERW tube mill should provide:
- Stable forming section
- Strong machine rigidity
- Accurate squeeze roll alignment
- Reliable HF welding system
- Low vibration during operation
These factors directly affect weld consistency.
Machine Performance vs Welding Stability
| Machine Condition | Welding Result |
|---|---|
| Poor rigidity | Unstable welding |
| Roll vibration | Inconsistent squeeze force |
| Poor alignment | Weak weld quality |
| Stable machine | Reliable weld performance |
At MIVI Tube Machine, machine design focuses heavily on welding stability.
This includes optimization of:
- Forming section rigidity
- Shaft precision
- Roll alignment
- Squeeze section stability
- High-frequency welding efficiency
The goal is simple.
Make welding more stable.
Reduce defects.
Improve production efficiency.
Why Customers Upgrade to MIVI Tube Mills
Many manufacturers contact MIVI for the same reason.
Their existing production line still runs.
But production quality becomes difficult to control.
Common complaints include:
- Frequent weld defects
- Hydro test failures
- Excessive burr
- Roller wear
- High maintenance cost
In many cases, the problem is not only welding parameters.
It is machine stability.
A better tube mill creates better welding conditions.
That makes process optimization much easier.
MIVI Advantages
✔ 20+ years manufacturing experience
✔ Precision machining
✔ Stable machine structure
✔ Reliable welding performance
✔ Lower maintenance cost
For manufacturers producing:
- Carbon steel pipes
- Round pipes
- Square tubes
- Structural pipes
machine stability becomes a major competitive advantage.
Conclusion
In ERW welding, many production issues appear to be electrical problems.
But after careful analysis, the root cause is often more complex.
Weld quality depends on balance.
Not just power.
Not just pressure.
The relationship between welding power and ERW squeeze force determines whether weld quality remains stable.
Too much power creates overheating.
Too little squeeze force creates weak bonding.
Too much pressure causes excessive burr and mechanical wear.
The best welding result comes from balancing three key factors:
- Welding power
- ERW squeeze force
- Production speed
When these parameters work together, manufacturers achieve:
- Stronger weld seams
- Lower defect rate
- Better production efficiency
- Lower operating cost
Stable welding is never accidental.
It comes from the right machine, the right process, and the right parameter control.
If your production line suffers from:
- Excessive sparks
- Weld seam cracking
- Hydro test failure
- Excessive burr
it may be time to evaluate both welding parameters and machine condition.
A professional diagnosis often reveals the real cause much faster.
Can increasing welding power solve weak weld problems?
Not always.
In many cases, increasing power only hides the real problem.
The root cause may be unstable squeeze force or poor machine alignment.