


 Tube Mill Consumables: Inspection & Replacement Guide




-
1. What is the material of the pipe that the machine produce
GI pipe, Steel pipe, Mild steel pipe, Low carbon steel pipe -
2. Is it possible to customize the equipment according to the demanding of the customer?
-
3. Do you have any certificates?
-
4. What is the payment method?
-
5. What does the after-service do you provide?
-
6. When will the engineer arrive?
-
7. How long will the installation and staff training?
-
8. Do you have reference project?
-
9. What about spare parts?
What Is the Best ERW Squeeze Force for Stable Tube Welding?
Power vs Squeeze Force in ERW Welding: Best ERW Squeeze Force for Stable Weld Quality
In ERW tube mill production, ERW squeeze force directly affects weld quality and welding stability.
If squeeze force is too low, strip edges cannot forge properly, leading to weak welds, cold welding, and hydro test failure. If squeeze force is too high, excessive burr, roller wear, and unstable weld seams become common.
The best welding condition is achieved when welding power and ERW squeeze force are balanced.
A proper balance helps manufacturers:
- Improve weld strength
- Reduce weld defects
- Lower scrap rate
- Increase production stability
This article explains how welding power and squeeze force interact, common welding problems, and how to optimize them for stable tube production.
| Condition | Common Problem | Result |
|---|---|---|
| Power too high | Overheating | Burned weld |
| Pressure too low | Weak forging | Cold weld |
| Over squeeze | Excessive upset | Large burr |
| Balanced settings | Stable welding | Strong weld |
What Happens When Welding Power Is Too High?
When welding power is too high, strip edges overheat before reaching the squeeze rolls.
This causes:
- Large sparks
- Burned weld seam
- Excessive oxidation
- Surface defects
Excessive heating prevents stable forging and weakens weld quality.
Stable heating depends heavily on your High Frequency Welding Machine
| Symptom | Cause | Solution |
|---|---|---|
| Large sparks | Excessive power | Reduce power |
| Burned seam | Overheating | Lower HF output |
| Oxidation | Excess heat | Optimize V-angle |
Why Does Low ERW Squeeze Force Cause Weak Welds?
When ERW squeeze force is too low, the heated strip edges cannot bond completely.
This leads to:
- Cold weld
- Weak seam bonding
- Oxide inclusion
- Hydro test failure
The weld may look normal externally, but internal bonding is poor.
| Problem | Root cause |
| Cold weld | Low squeeze force
|
| Weak seam | Insufficient forging |
| Hydro failure | Poor bonding |
Stable pressure control requires a reliable ERW Tube Mill Machine
What Problems Does Over Squeeze Cause?
Too much squeeze force can also reduce weld quality.
Over squeezing causes:
- Excessive burr
- Large weld upset
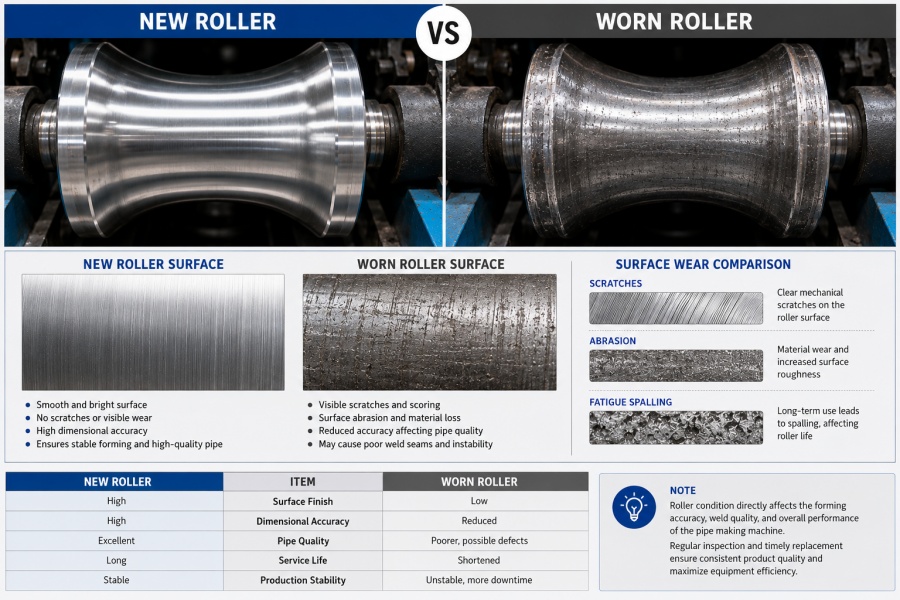
- Roller wear
- Bearing overload
Many operators assume higher pressure improves welding, but excessive force often creates instability.
| Problem | Effect |
|---|---|
| Large burr | Material waste |
| Roller wear | Higher maintenance |
| Bearing load | Shorter machine life |
Worn [Tube Mill Mould] and squeeze rolls also affect pressure consistency.
What Is the Best ERW Squeeze Force for Stable Welding?
The best ERW squeeze force depends on:
- Tube diameter
- Wall thickness
- Material grade
- Production speed
- Welding power
There is no universal setting.
The goal is to achieve:
✔ Proper heating
✔ Stable forging
✔ Clean weld seam
✔ Consistent production
Best Balance Table
| Parameter | Ideal Condition |
|---|---|
| Welding Power | Stable heating |
| Squeeze Force | Proper forging |
| Line Speed | Balanced production |
How Can You Test ERW Weld Quality?
Reliable testing is essential for weld quality verification.
Three major methods are used.
Hydro Test
Checks:
- Leakage
- Seam cracks
Flattening Test
Checks:
- Ductility
- Weld strength
UT Inspection
Checks:
- Internal defects
- Lack of fusion
Inspection Table
| Test | Detects |
| Hydro Test | Leakage |
| Flattening Test | Cracks |
| UT Inspection | Internal defects |
How Can You Improve ERW Welding Stability?
1. Process Optimization
- Improve V-angle
- Check impeder
- Adjust coil position
2. Parameter Optimization
- Balance power
- Optimize speed
- Adjust squeeze force
3. Equipment Upgrade
- Improve roll rigidity
- Reduce vibration
- Increase alignment precision
Solution Table
| Solution | Benefit |
|---|---|
| Process optimization | Better welding |
| Parameter optimization | Stable weld |
| Equipment upgrade | Lower defects |
Which Tube Mill Machine Is Best for Stable ERW Welding?
For stable ERW welding, machine rigidity and squeeze roll precision are critical.
A reliable tube mill should provide:
- Stable forming section
- Accurate squeeze alignment
- Reliable HF welding
- Low vibration
MIVI tube mills are designed to improve:
- Weld consistency
- Production efficiency
- Machine lifespan
Conclusion
ERW squeeze force is one of the most important factors in weld quality.
In most cases:
- High power causes overheating
- Low pressure causes weak welds
- Over squeeze causes burr and roller wear
The best results come from balancing:
- Welding power
- ERW squeeze force
- Production speed
Optimizing these three factors is the key to stable tube mill production.
FAQ
What is ERW squeeze force?
ERW squeeze force is the pressure applied by squeeze rolls to forge heated strip edges together.
Why is squeeze force important in ERW welding?
It directly affects weld strength, weld stability, and defect rate.
What happens if squeeze force is too high?
It causes excessive burr, roller wear, and unstable welding.
What happens if squeeze force is too low?
It leads to cold welds, weak seams, and hydro test failure.