


 Tube Mill Consumables: Inspection & Replacement Guide



Why Flattening Test Failure Happens in Steel Pipe Production
A pipe can pass visual inspection and still fail badly a few minutes later.
That happens more often than many factories want to admit.
The surface looks clean.
The weld line seems normal.
Production speed is stable.
Then the flattening test starts.
Pressure increases slowly, and suddenly the weld seam opens. Sometimes it is just a small crack near the edge. Sometimes the whole seam splits apart.
In many ERW pipe plants, this is where hidden welding problems finally show themselves.
The flattening test is not just another quality procedure. It is one of the fastest ways to expose weak fusion, unstable welding temperature, poor squeeze pressure, or strip defects that were already there during forming.
Factories producing carbon steel tubes for construction, furniture, scaffolding, and water pipe applications deal with this issue regularly, especially when production speed increases or raw material quality changes from batch to batch.
Modern production lines try to reduce these failures through better strip preparation, stable forming, and more accurate squeeze control. This is one reason many manufacturers are upgrading to newer Carbon Pipe Manufacturing Machine systems instead of relying on older manual adjustment lines.
What Exactly Is a Flattening Test?
The principle is simple.
A short section of welded pipe is placed between two flat plates and compressed gradually until a specified distance is reached.
The goal is not to destroy the pipe for no reason.
The test checks whether the weld area can withstand deformation without cracking.
If the seam splits early, the problem is usually deeper than appearance alone.
According to industrial flattening standards, the process is mainly used to evaluate weld ductility and detect hidden seam defects that cannot always be identified visually.

Why Some Pipes Fail the Test
This part is where many factories lose money without realizing the real reason.
People often blame operators first.
But in actual production, flattening cracks are usually connected to several smaller problems happening together.
Not one single issue.
Unstable Welding Heat
If the welding temperature is too low, the strip edges never fully fuse.
The weld may still look acceptable from outside, especially at high line speed. But internally, weak bonding remains inside the seam.
Once compression begins during flattening, that weak area becomes the starting point of the crack.
Too much heat is not good either.
Overheating can create brittle structures around the weld zone, which later crack under pressure.
This becomes more obvious in thinner wall pipes running at high speed.

Strip Edge Problems
A lot of flattening failures actually begin before welding starts.
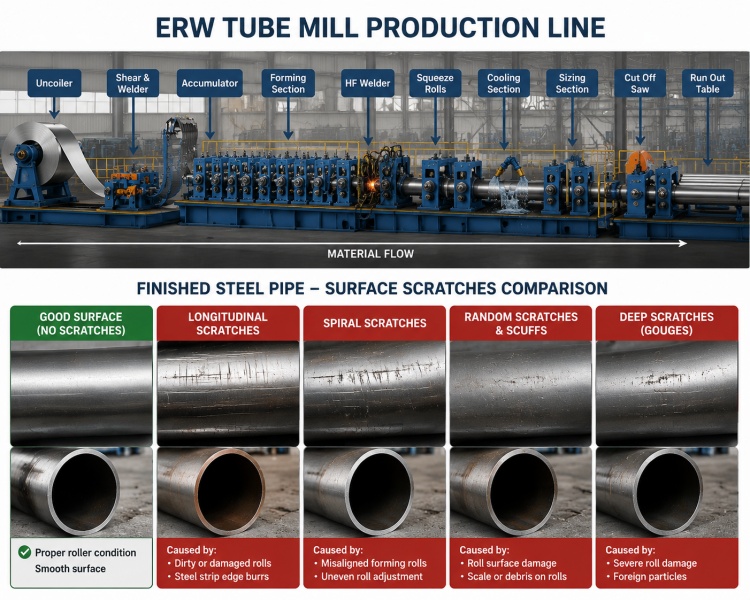
If strip edges contain burrs, waviness, residual stress, or poor trimming quality, the weld seam becomes unstable immediately.
That is why modern leveling and flattener systems are becoming more important in newer ERW lines.
Some newer leveling units are specifically designed to remove edge waves and residual stress before forming so the strip enters the welding section more evenly.
You can also see this issue more frequently when steel suppliers change material sources without stable chemical composition control.
Phosphorus segregation and inclusions can increase brittleness around the weld area and make flattening performance much worse.
Squeeze Pressure Problems
Another common issue is improper squeeze adjustment.
Too little squeeze pressure leaves incomplete bonding.
Too much pressure may damage the weld structure itself.
Older mills often rely heavily on operator experience for adjustment, so production stability changes between shifts.
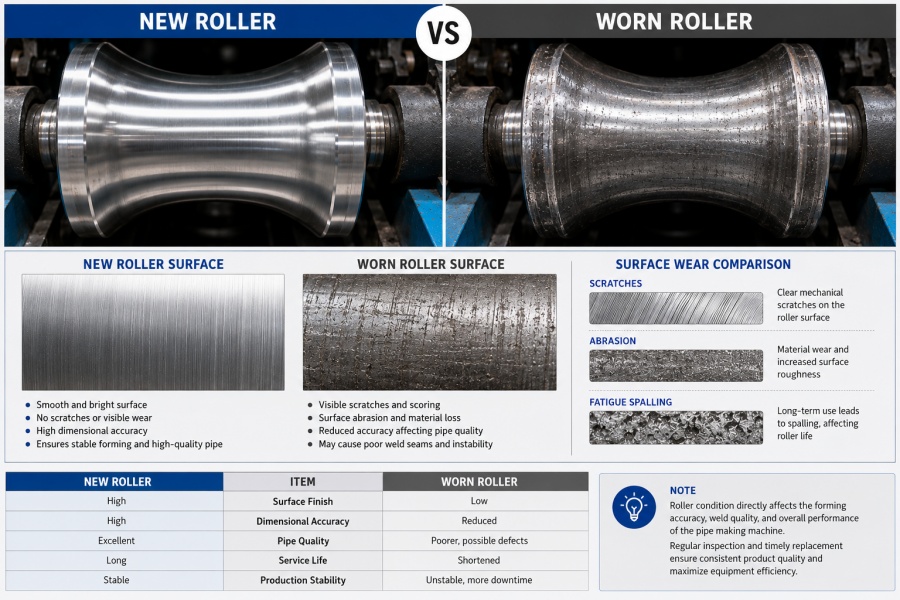
This becomes very noticeable on aging production lines where roller wear and bearing movement already affect alignment.

Why Modern Equipment Makes a Difference
Some factories continue adjusting welding parameters every day but still cannot stabilize flattening results.
The reason is simple.
If the forming section itself is unstable, welding consistency becomes difficult no matter how experienced the operator is.
Newer ERW production lines focus much more on:
- strip stability
- forming precision
- automatic squeeze adjustment
- stable V-angle control
- better welding consistency
Several newer tube mill systems now integrate leveling, forming, welding, sizing, and online inspection more tightly to reduce variation during production.
A stable Carbon Pipe Manufacturing Machine does not completely eliminate defects overnight, but it usually reduces hidden weld problems significantly compared with older lines that depend heavily on manual correction.

A Small Crack Usually Means a Bigger Problem
Flattening failure is rarely an isolated event.
If cracks appear during testing, there is a good chance similar instability already exists somewhere else in the production process.
Sometimes the next problem becomes hydro test leakage.
Sometimes customers discover seam cracking during bending or fabrication.
That is why experienced tube manufacturers usually treat flattening rejection as an early warning sign, not just a testing issue.
Improving weld quality often starts with basic things:
- better strip preparation
- stable forming alignment
- proper squeeze force
- cleaner welding conditions
- more consistent machine control
And in many cases, upgrading older production equipment becomes cheaper than continuously dealing with scrap, rework, and customer complaints.
If flattening cracks are becoming more frequent in your production line, it is usually a sign that weld consistency is already unstable somewhere in the process.
A more stable forming section, better squeeze control, and a modern tube mill setup can reduce rejection rates significantly.
You can explore more about our Carbon Pipe Manufacturing Machine Solutions for ERW steel pipe production.